| No. | Light Source Type | Wavelength (nm) | Operating Mode | Typical Power Range | Cleaning Mechanism | Cleanable Substrates | Typical Contaminant Layer / Cleaning Target | Target Industries | Suitability Level | Key Process Notes & Risks |
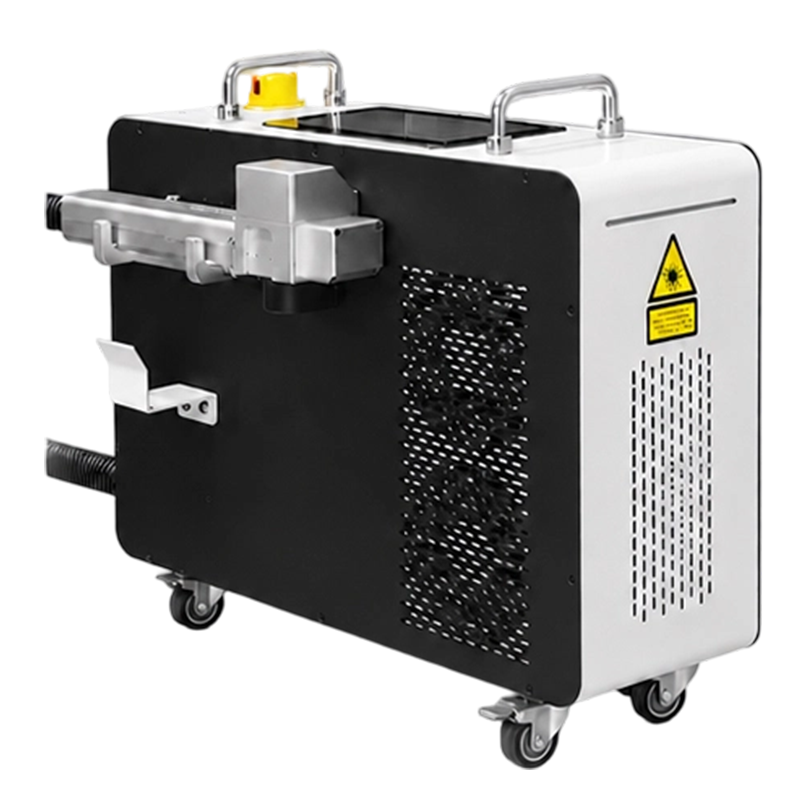
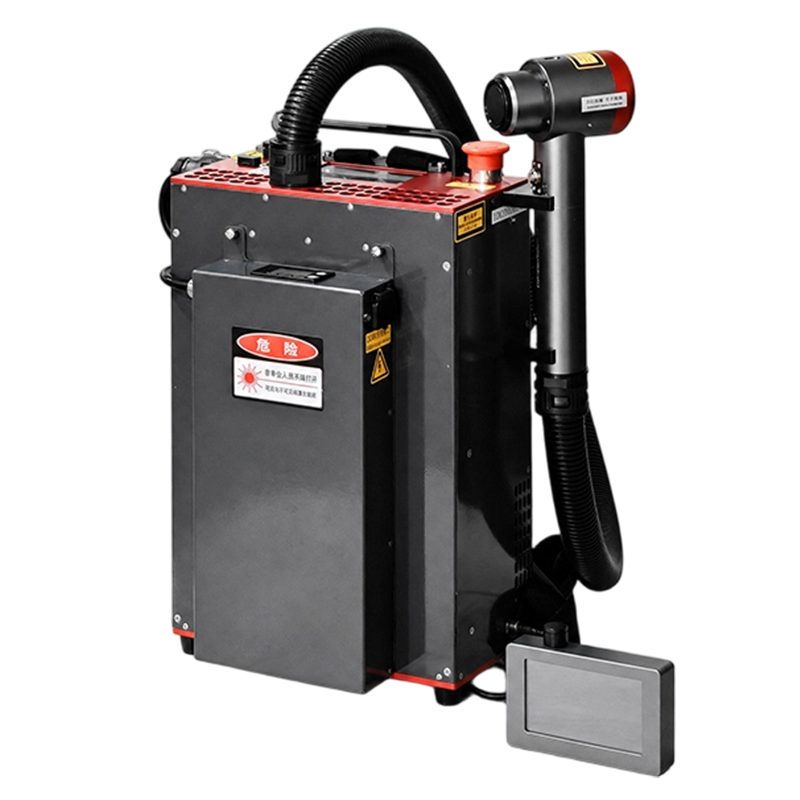
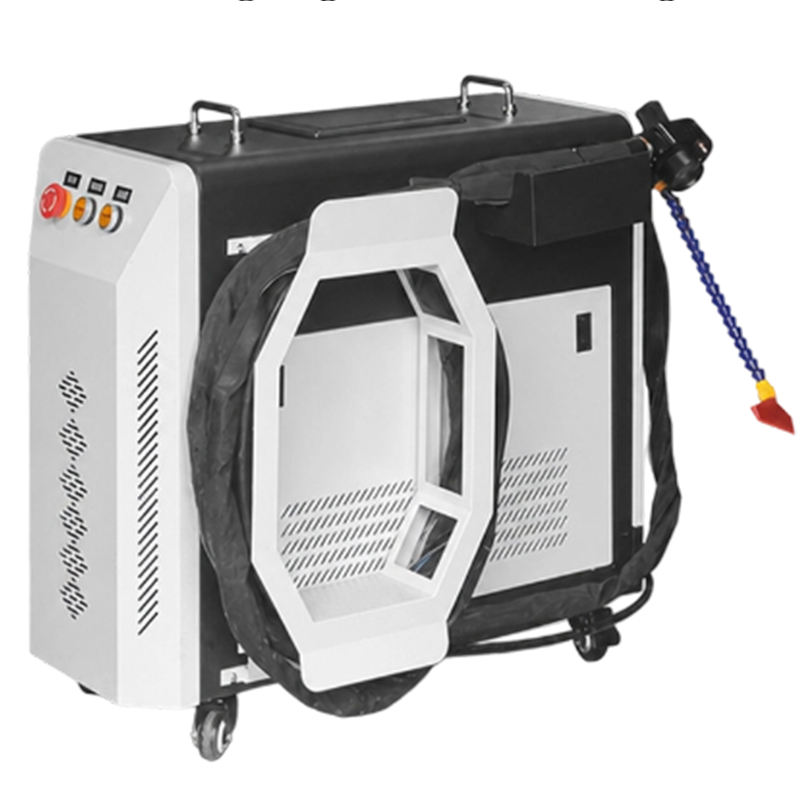
| 1 | Pulsed Laser Cleaning Machine | 1064 | Nanosecond Pulsed | 100 / 200 / 300 / 500 / 1000 W | High-peak-power pulses instantly vaporize the contaminant layer and shear it off by shock wave; the metal substrate absorbs little average energy | Carbon steel, low-alloy steel, cast iron | Flash rust, thick mill scale, old paint, oil and grease | Shipbuilding & repair, steel bridges, construction machinery, rail transit, heavy equipment | Preferred | Industry workhorse; for thick rust use 300 W or above with a wide galvo or line beam; carbon steel tolerates high energy, but watch thin-plate distortion |
| 2 | Pulsed Laser Cleaning Machine | 1064 | Nanosecond Pulsed | 200 / 300 / 500 W | As above; peak power density must exceed the oxide-layer threshold | Stainless steel | Weld discoloration, spatter, HAZ darkening, drawing oil | Food machinery, pharmaceutical equipment, kitchenware, decorative tubing | Preferred | Post-weld cleaning needs energy control to avoid yellowing or dulling of the substrate; use MOPA short pulses on mirror-finish parts |
| 3 | Pulsed Laser Cleaning Machine | 1064 | Nanosecond Pulsed | 300 / 500 / 1000 W | Fast thermo-mechanical coupling removal; line beam improves coverage | Weld beads and heat-affected zone (steel / aluminum / titanium) | Post-weld oxide scale, spatter, slag, fume deposits | Automotive body-in-white, EV battery trays, sheet-metal enclosures, pipe prefabrication | Preferred | One machine for both pre-weld and post-weld cleaning; sharing a rail with the welding robot is the mainstream integration today |
| 4 | Pulsed Laser Cleaning Machine | 1064 | Nanosecond Pulsed | 200 / 300 / 500 W | Dry ablation, no abrasion, no consumables; does not damage mold surface accuracy | Tire molds, rubber molds, injection molds, die-casting dies | Cured rubber residue, carbon buildup, release agent, pigment powder | Tire manufacturing, rubber and plastics, injection molding, die casting | Preferred | The most mature retrofit case for laser cleaning; match a 3D galvo or robot arm to the mold cavity depth |
| 5 | Pulsed Laser Cleaning Machine | 1064 | Nanosecond Pulsed | 100 / 200 W | Low single-pulse energy with multiple passes to avoid melting the substrate | Aluminum alloy, die-cast aluminum, magnesium alloy (risk) | Oxide film, release agent, cutting oil, pre-weld surface preparation | Automotive lightweight parts, 3C structural parts, die casters | Restricted | Aluminum absorbs 1064 nm poorly and conducts heat fast: high power density is required but over-burning and whitening is easy; always run sample tests to fix parameters; magnesium alloy needs inert shielding |
| 6 | Pulsed Laser Cleaning Machine | 1064 | Nanosecond Pulsed | 100 / 200 W | Layer-by-layer ablation; can stop midway to preserve the under-plating | Galvanized sheet, coil-coated sheet, anodized parts | Local mark / coating removal, spot-weld site cleaning | Home appliances, building materials, elevators, curtain walls | Restricted | Zinc has a low boiling point and is easily damaged, leading to later corrosion; use point cleaning only, not area cleaning |
| 7 | Pulsed Laser Cleaning Machine | 1064 | Nanosecond Pulsed | 200 / 300 W | Non-contact, avoids abrasive wear on heritage surfaces | Stone, white marble, masonry, concrete | Dust, soot layer, graffiti, mold stains, weathering crust | Heritage restoration, historic building maintenance, municipal landscaping | Usable | Requires low energy, a large spot and progressive multi-pass cleaning; dark stone tends to show a visible “brightened” color shift |
| 8 | MOPA Variable-Pulse-Width Fiber Laser Cleaning Machine | 1064 | Pulsed (1–500 ns adjustable) | 60 / 100 / 200 / 300 W | Pulse width decoupled from peak power: short pulses give “cold ablation”, long pulses give thermal ablation | Thin sheet, precision hardware, plated parts, anodized aluminum | Thin rust, anodized layer, local coating removal, degreasing of precision parts | 3C electronics, precision hardware, connectors, medical devices | Preferred | The default choice for precision cleaning; at equal power, shorter pulses are gentler on the substrate but removal efficiency drops |
| 9 | MOPA Variable-Pulse-Width Fiber Laser Cleaning Machine | 1064 | Pulsed | 100 / 200 W | Short pulse width plus low single-pulse energy keeps the heat-affected zone at micron scale | Thin stainless parts, small copper-alloy parts, titanium-coated parts | Discoloration, fingerprints, micro burrs, local plating | Precision instruments, watch components, semiconductor packaging parts | Preferred | Suited to small-area, high-value parts; throughput is not its strength — yield is |
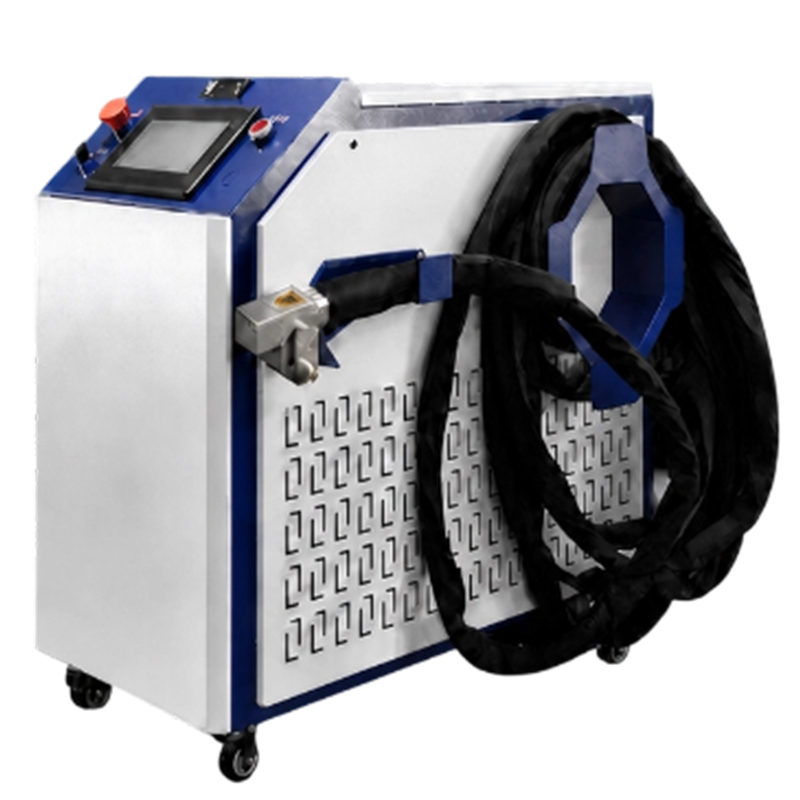
| 10 | Continuous-Wave (CW) Laser Cleaning Machine | 1070 | CW / Quasi-CW | 500 / 1000 / 2000 / 3000 W | Continuous heat input makes thick contamination burn, crack and spall, combined with high-speed scanning | Heavily rusted carbon steel, ship hull plate, large H-beam | Thick rust, multi-layer marine paint, old coatings | Shipbuilding & repair, offshore engineering, bridge steel structures, wind turbine towers | Preferred | Highest efficiency for large-area rough cleaning; high heat input distorts thin plate (<3 mm), so control overlap and dwell time |
| 11 | Continuous-Wave (CW) Laser Cleaning Machine | 1070 | CW / Quasi-CW | 1000 / 2000 W | Large spot with fast scanning; thermal stress breaks down the dirt | Concrete, stone, asphalt pavement | Dirt, graffiti, oil stains, old road markings | Municipal maintenance, building renovation, road works | Usable | Causes surface roughening; use with caution on stone where appearance matters |