Platform Large-Format Pulse Laser Cleaning Machine for Stainless Steel, Carbon Steel and Aluminium Moulds
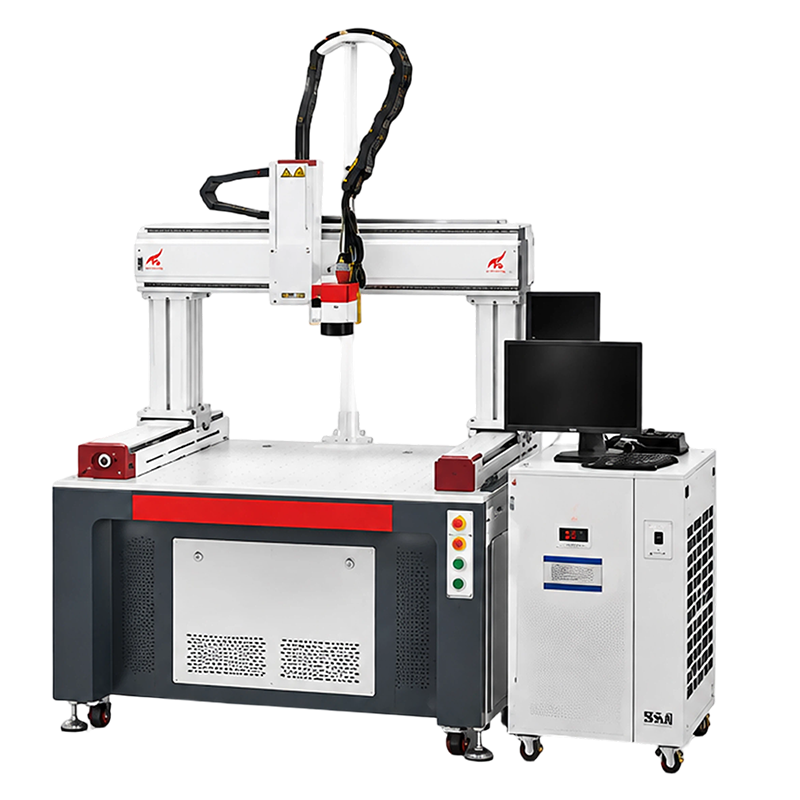
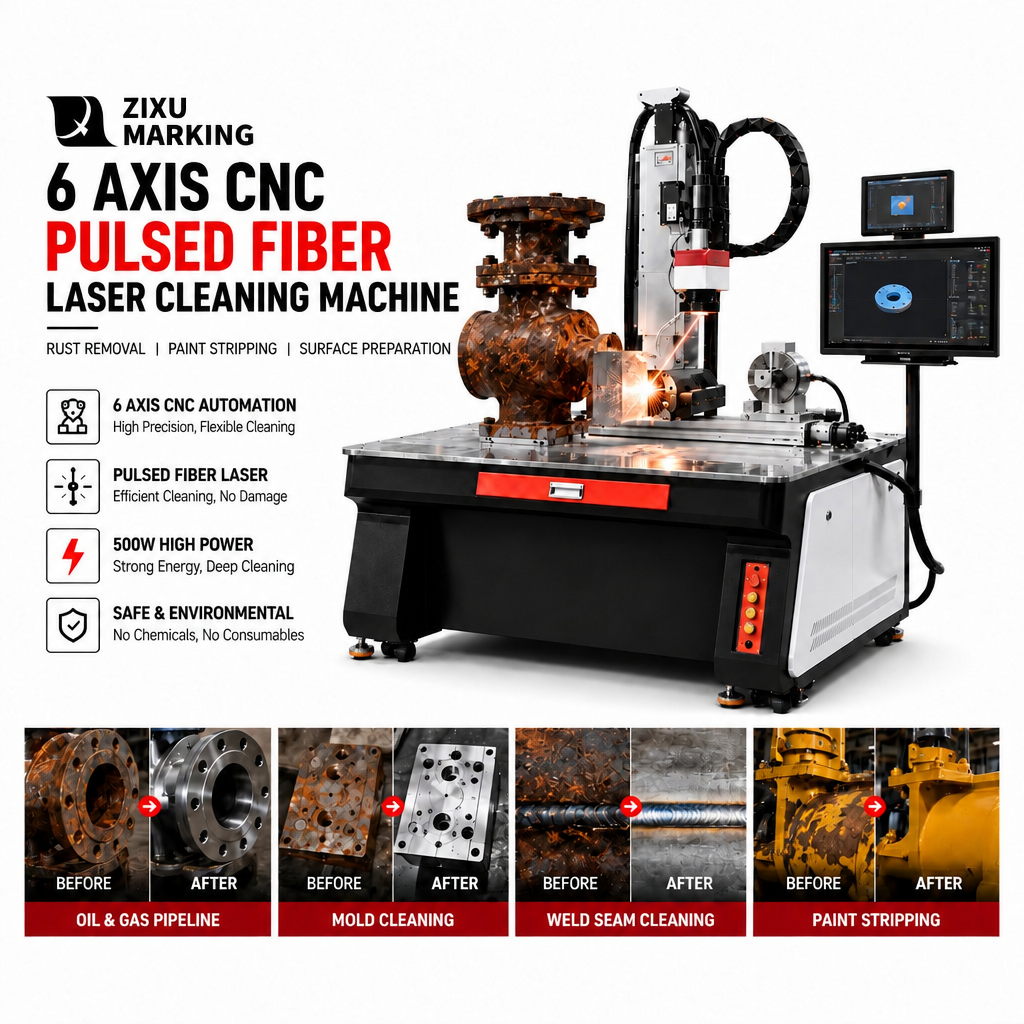
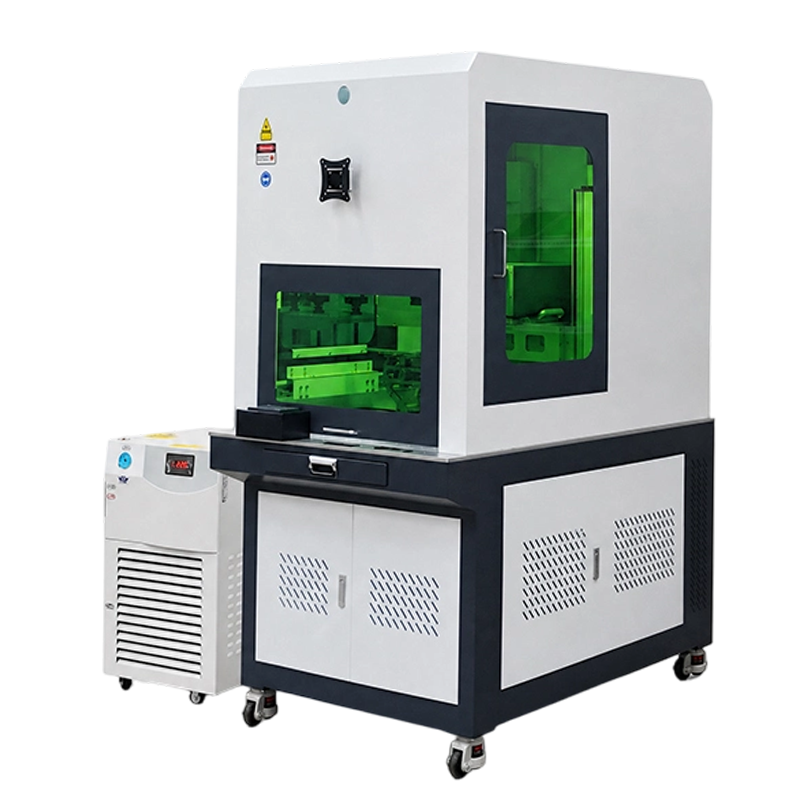
A gantry platform pulse laser cleaner: 1200×1200 mm table, 100-1000 W, path and energy locked by program, +/-0.01 mm repeatability, over 30 m2/h, Sa2.5/Sa3.
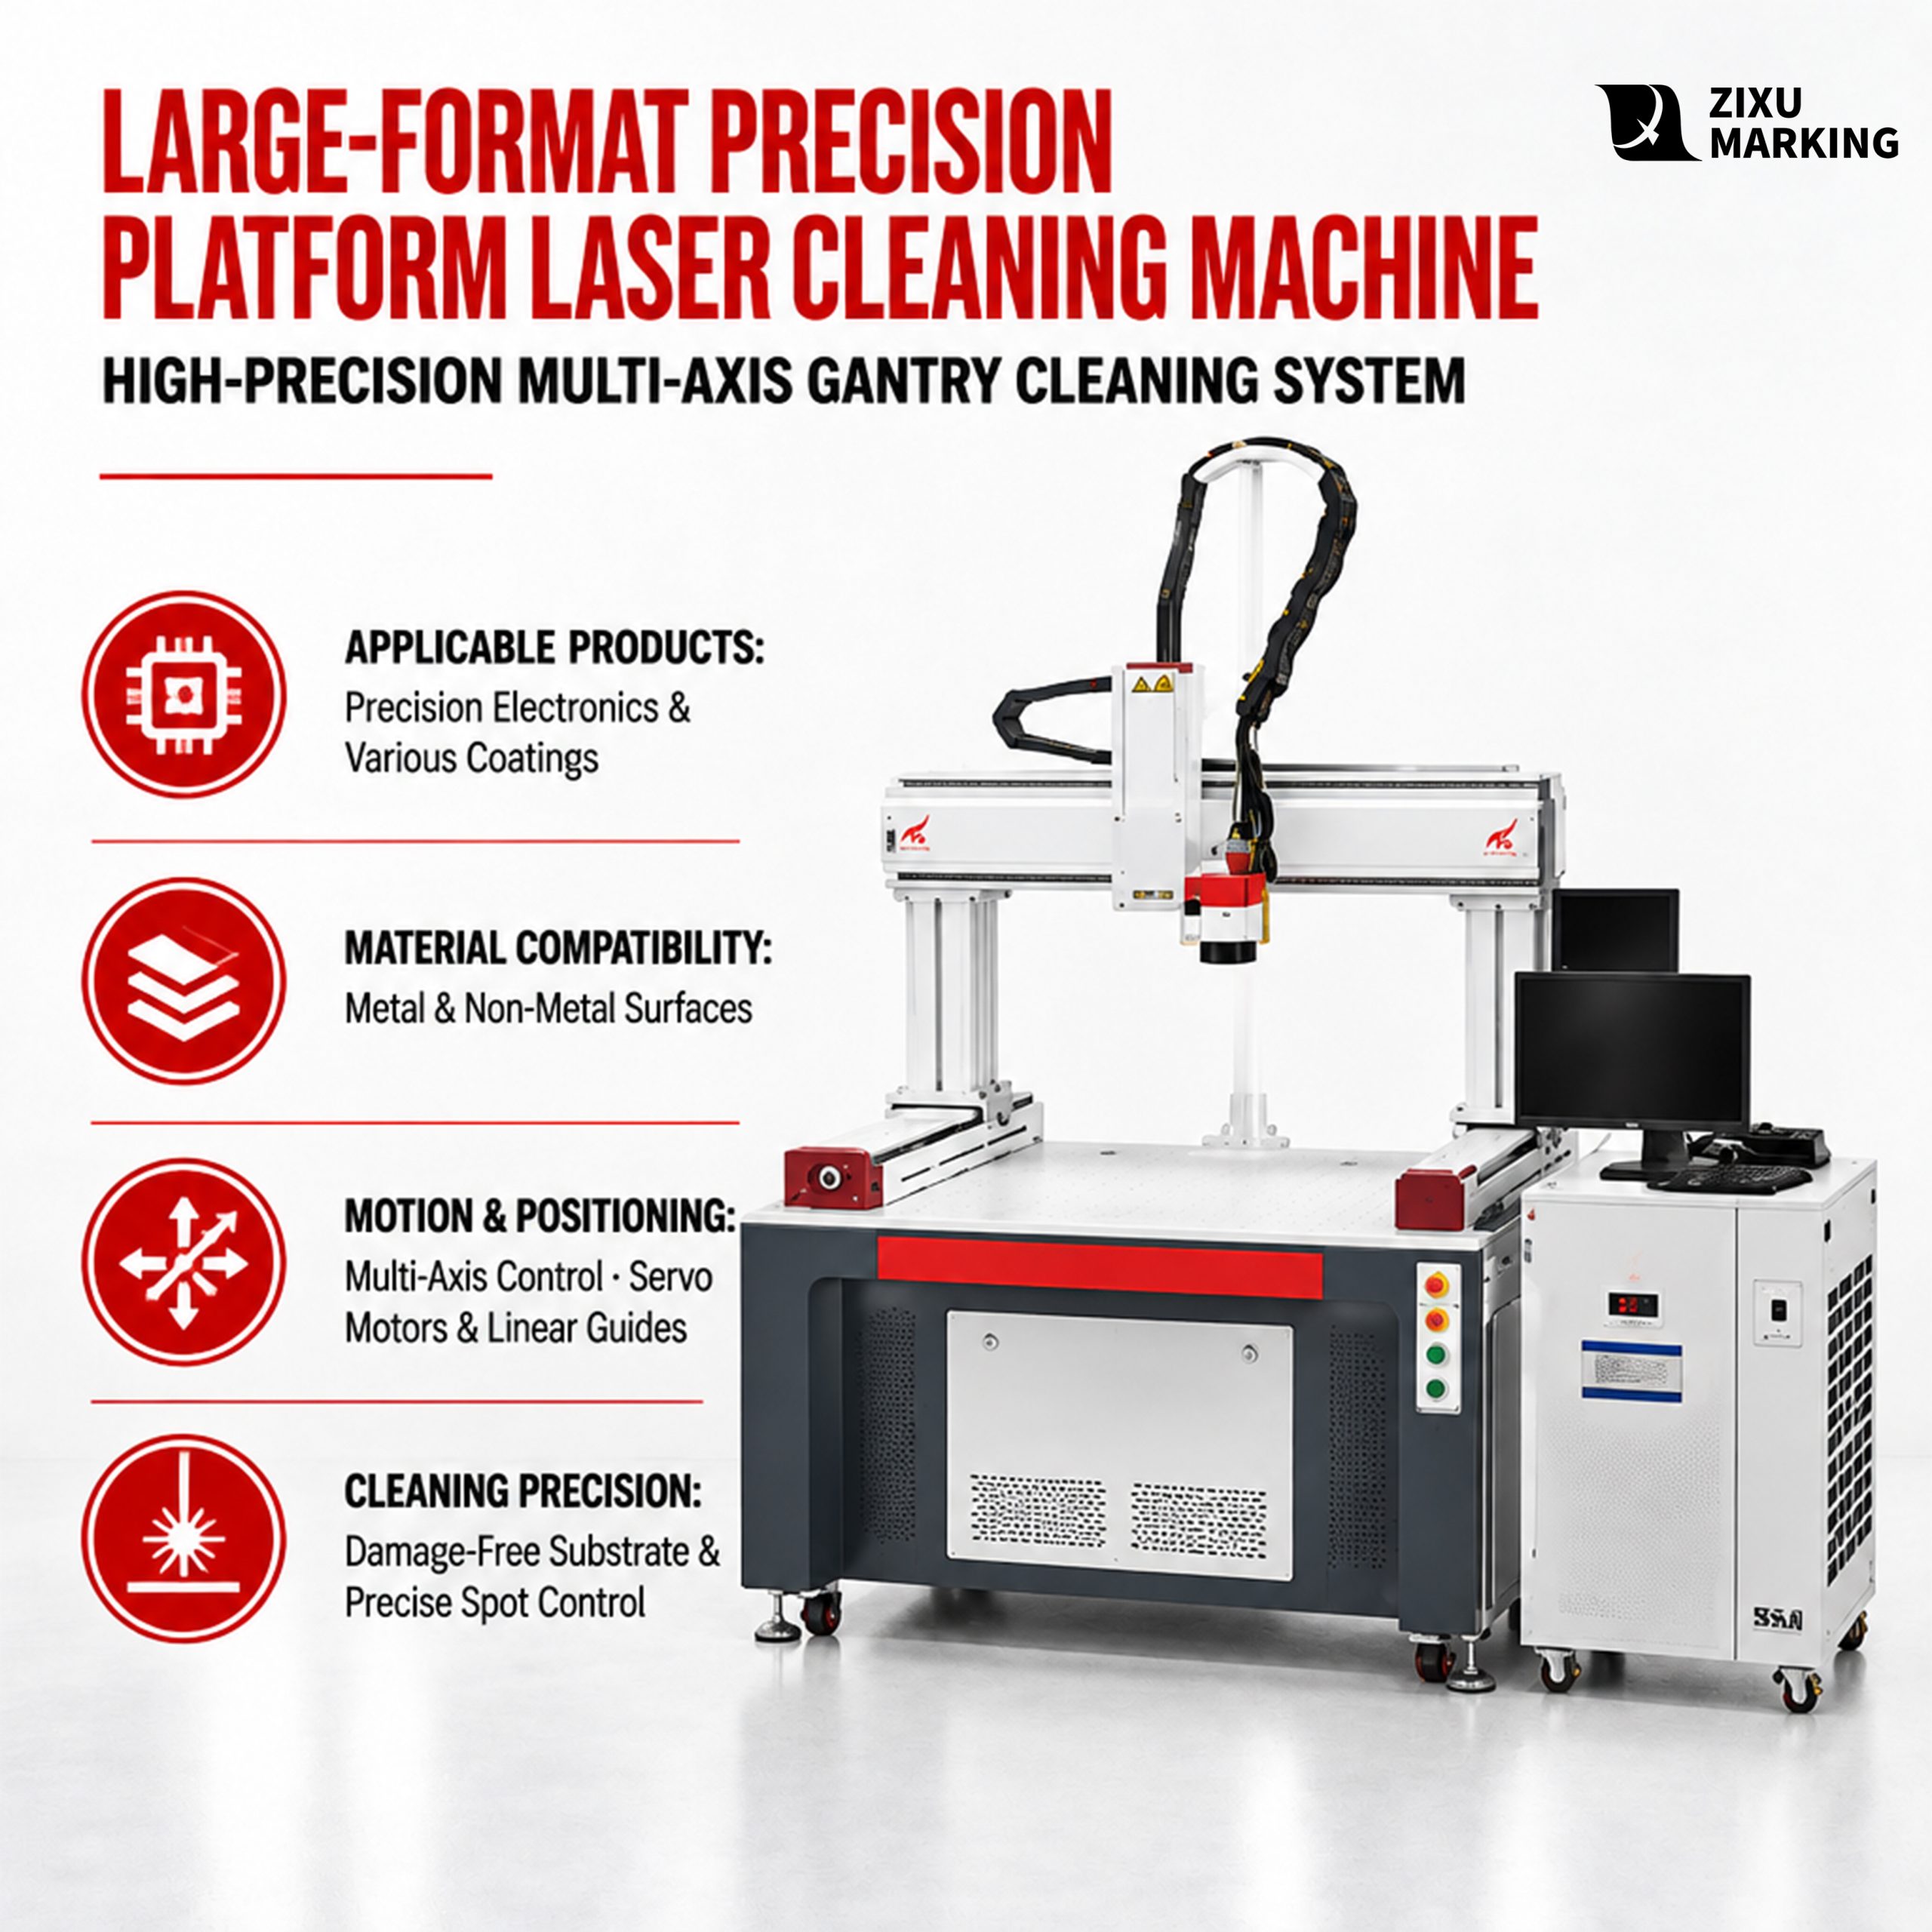
100 / 200 / 250 / 300 / 500 / 1000 W at 1080 nm, pulse width 30-500 ns and repetition 1-4000 kHz both adjustable, single pulse 1.5-100 mJ. Thin oxide wants low power at high repetition; heavy rust and old paint want the opposite. They are two separate dials.
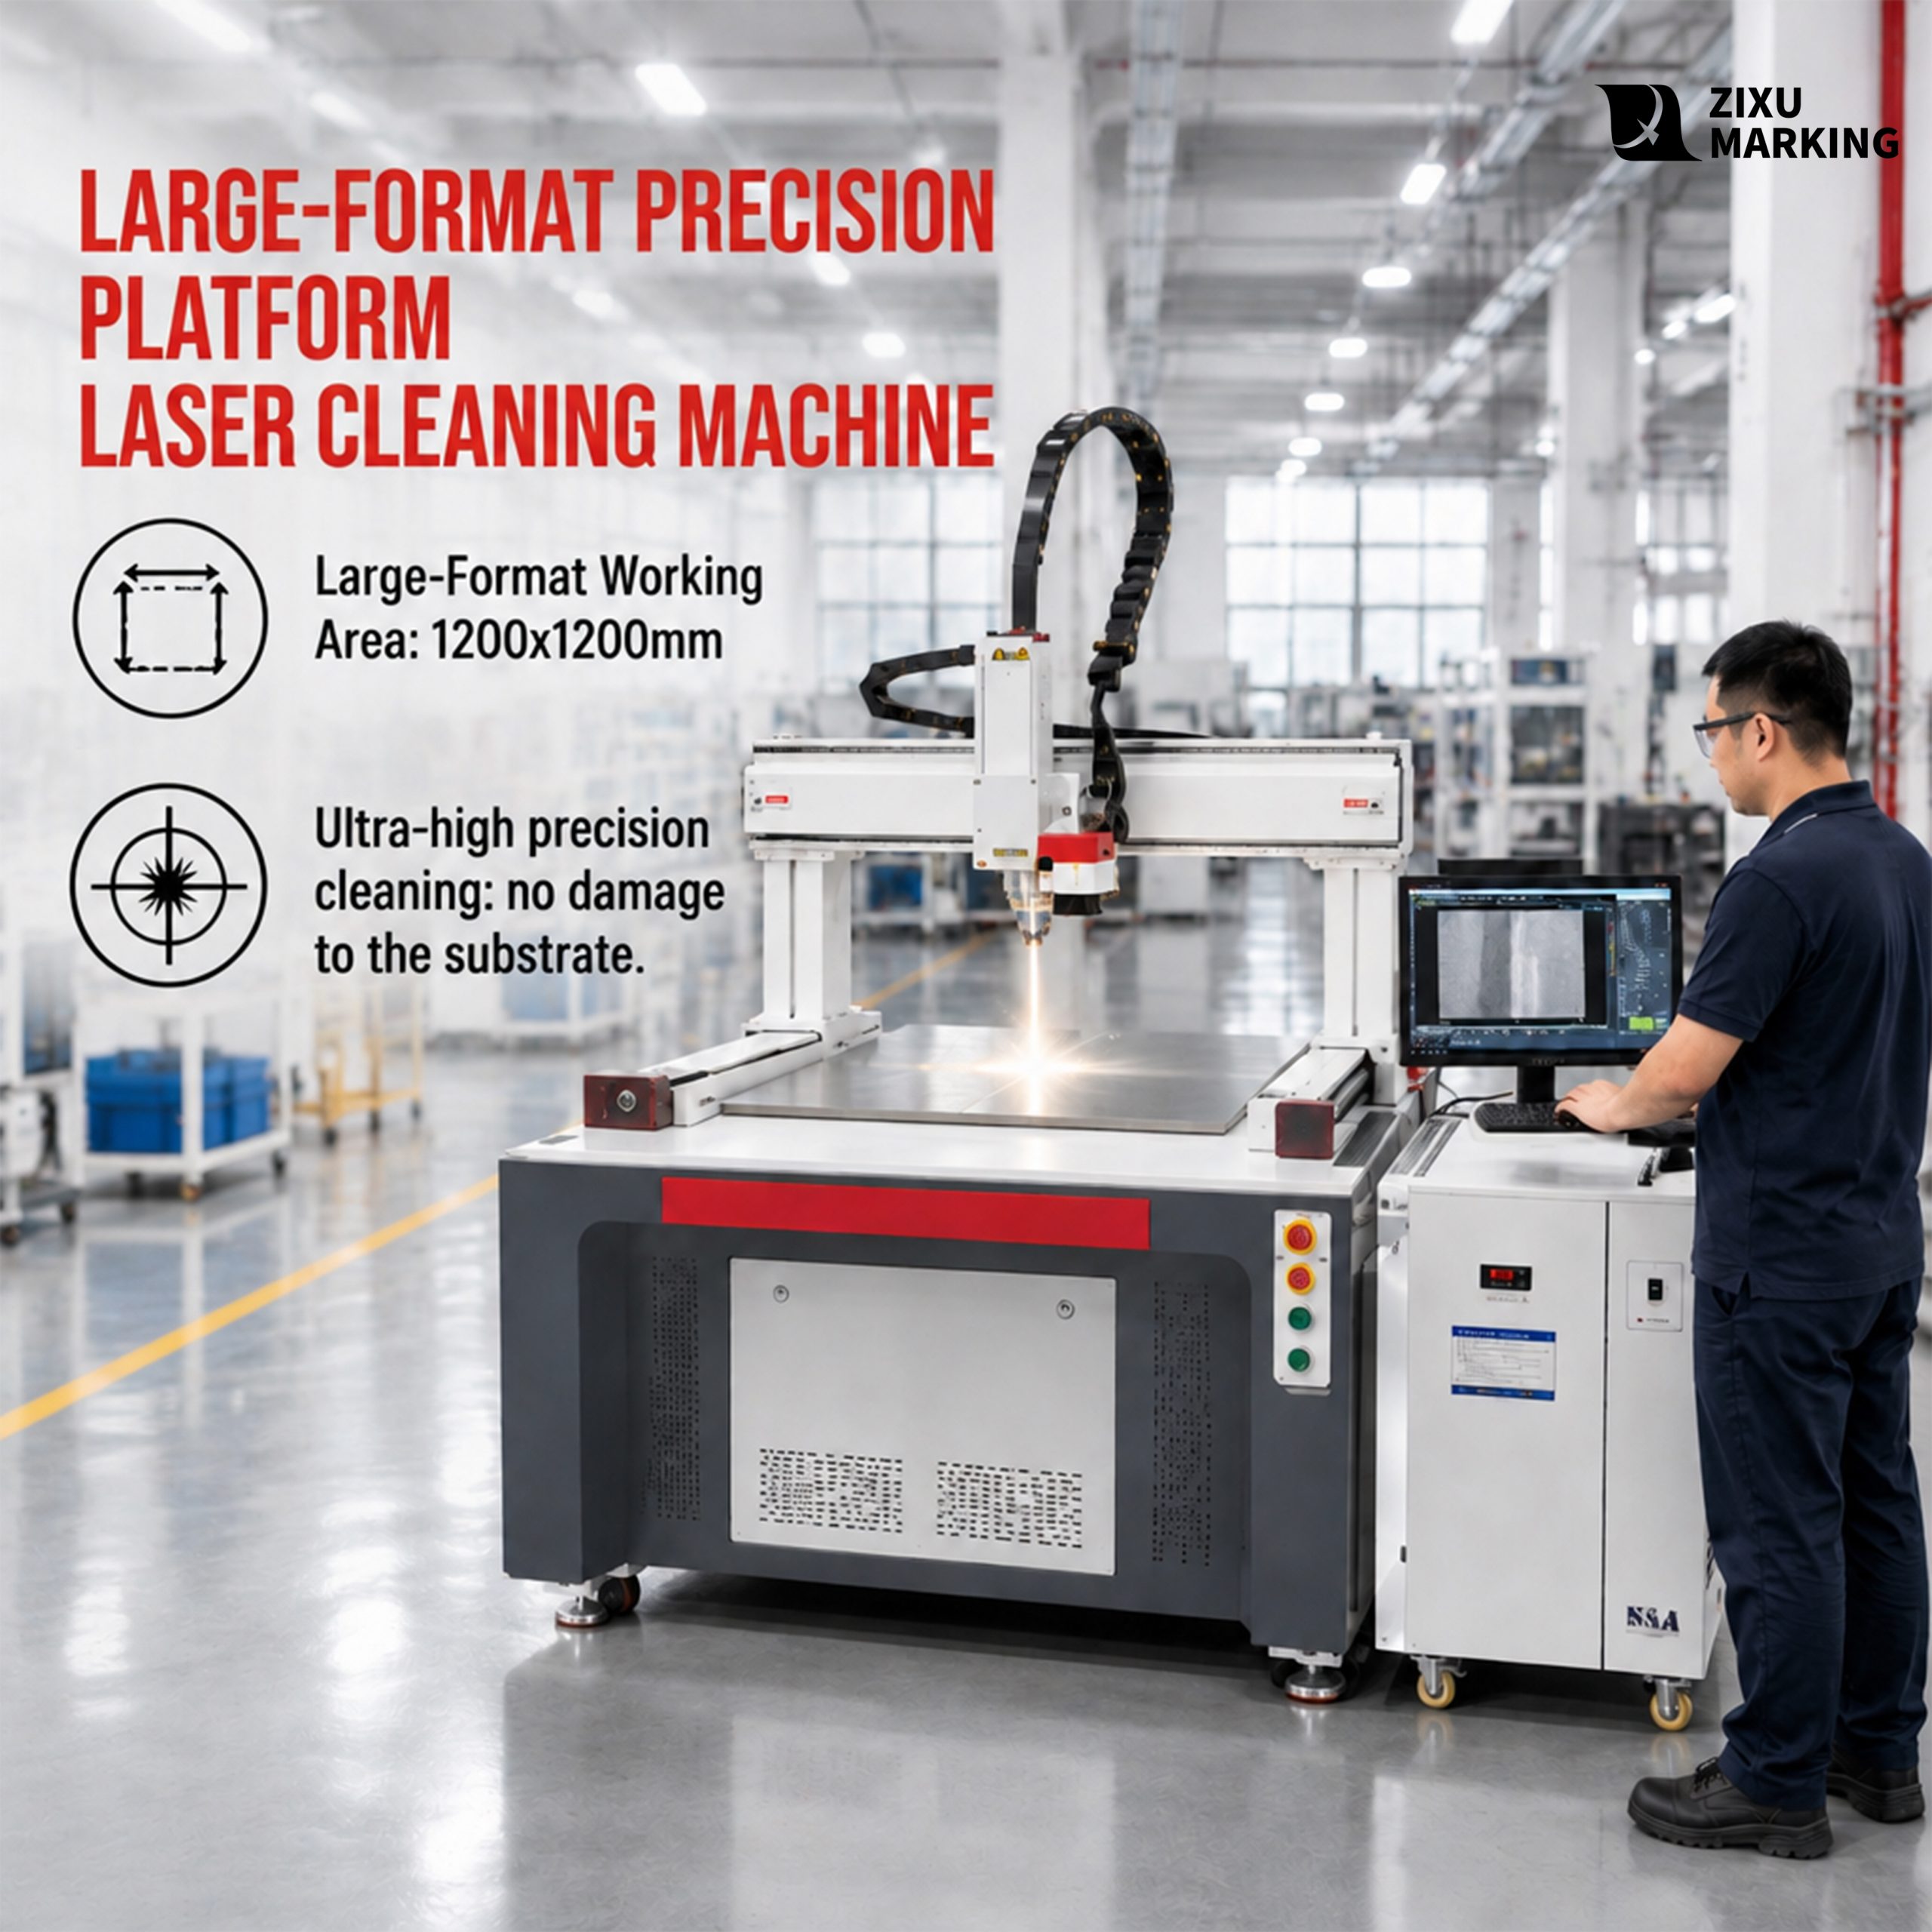
A 1200×1200 mm table as standard and larger to order, cleaning above 30 m2/h, and a finish graded Sa2.5 to Sa3 – the same grade a blasting specification asks for, which means the part can go straight into coating without a second inspection.
A dual-drive gantry with linear guides on X/Y and a ball screw on Z holds +/-0.01 mm. Three axes are standard; five or six are specified per workpiece – the rotary and tilt axes are what let the head clean a cavity wall or a slope normal to the surface.
ðLO 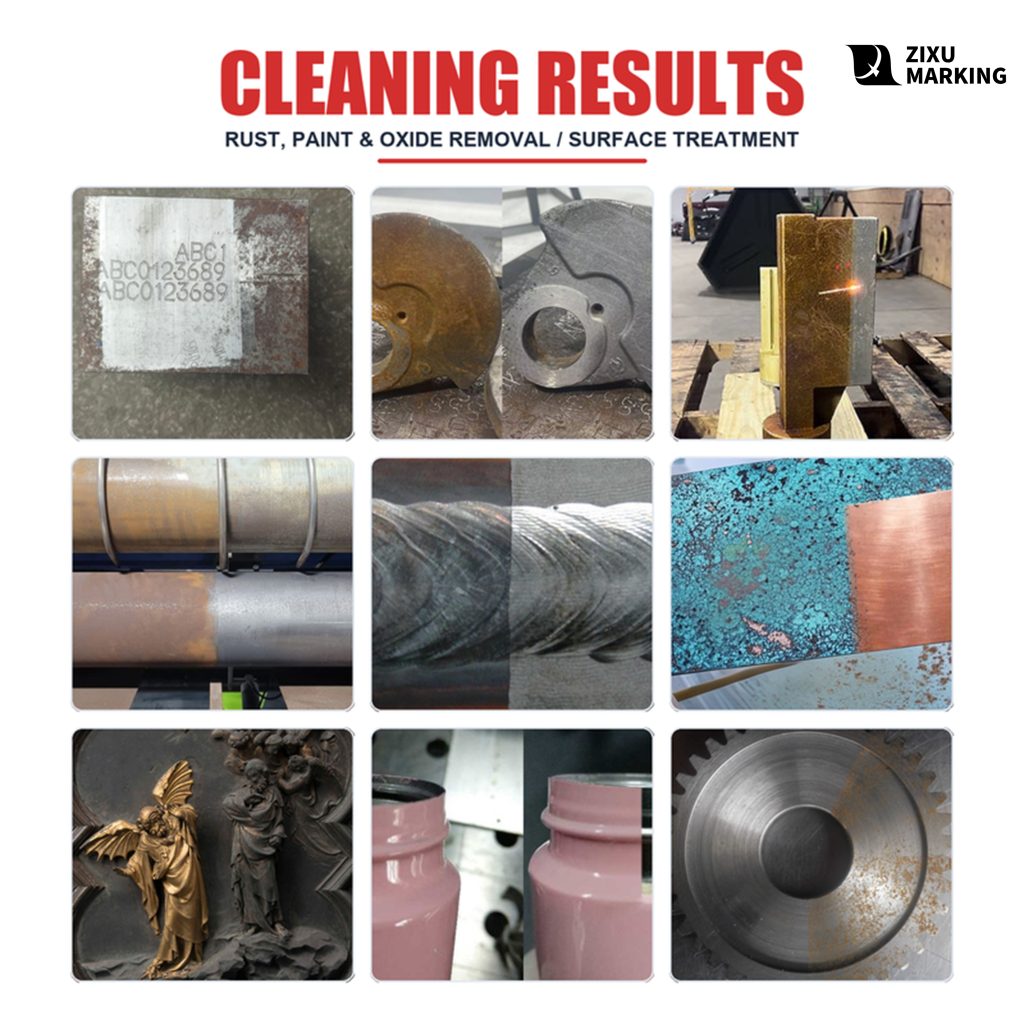
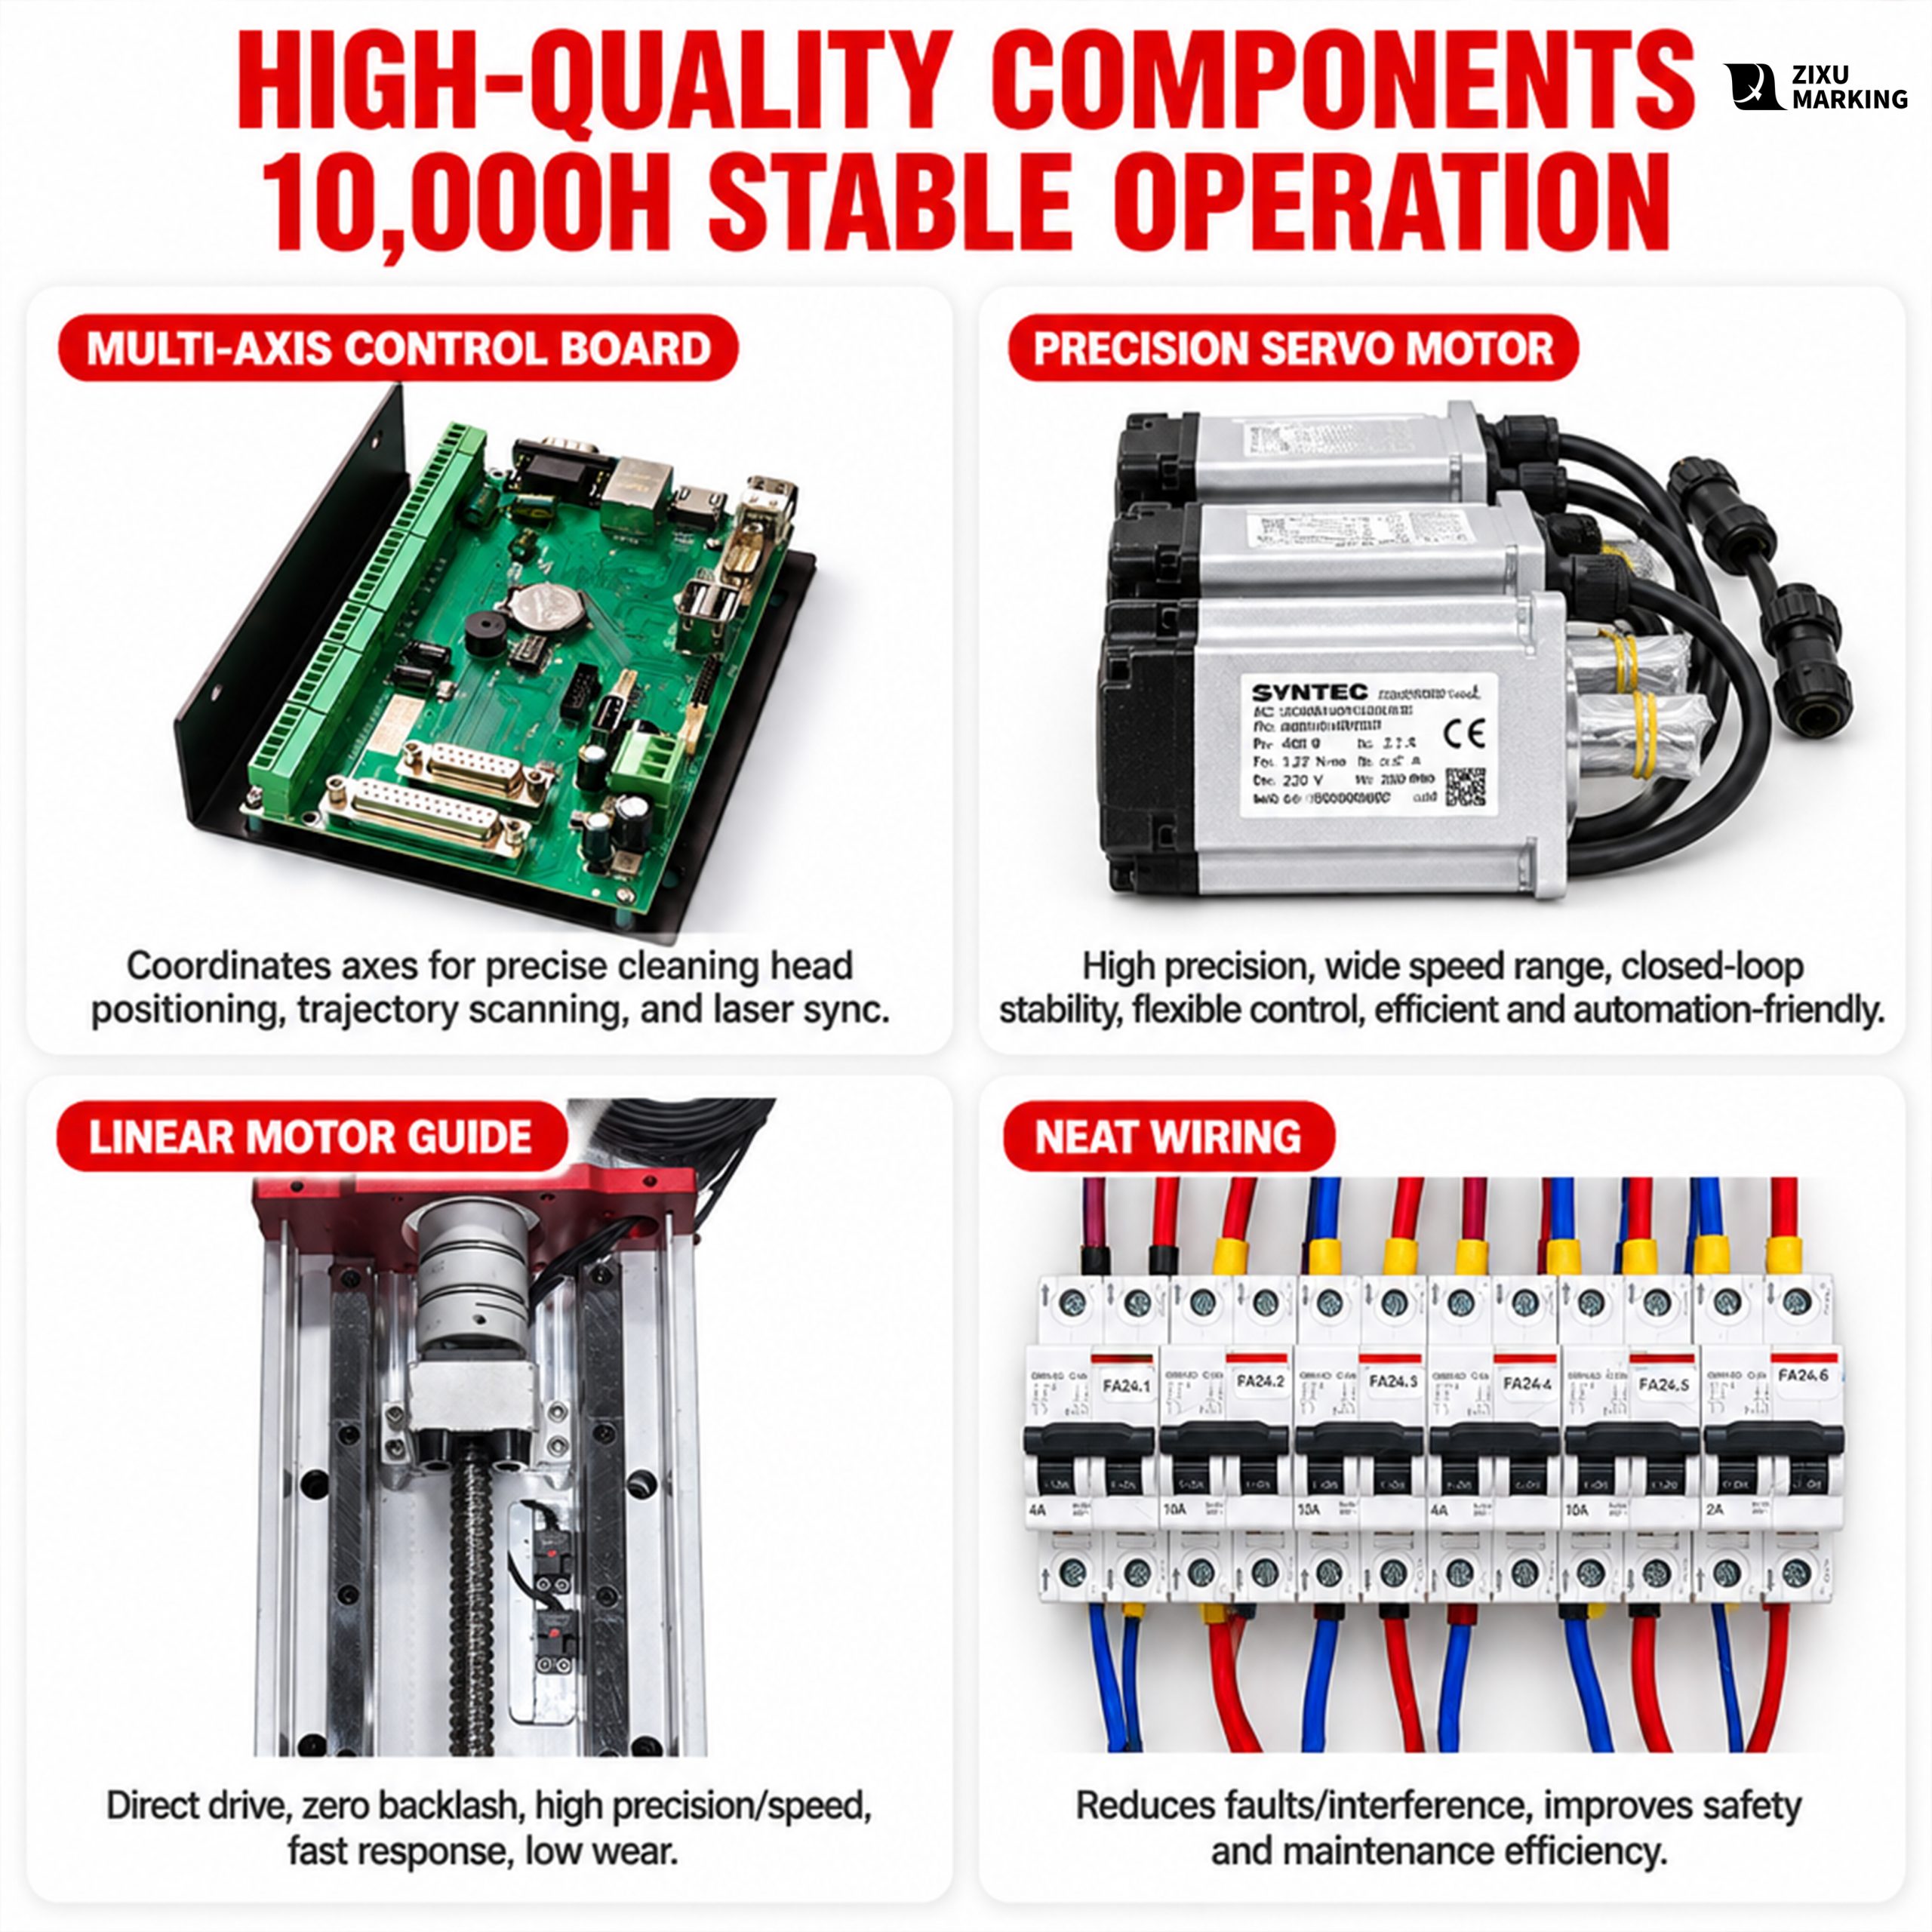
Gantry platform pulse laser cleaner: 1200×1200 mm table, 100-1000 W at 1080 nm, JPT source, HIWIN/THK/PMI rails, Panasonic/Yaskawa servos, +/-0.01 mm repeatability, over 30 m2/h, Sa2.5/Sa3.
| Group | Parameter | Value |
| A Optics | Laser Type | Pulsed Fiber Laser |
| A Optics | Rated Power | 100 / 200 / 250 / 300 / 500 / 1000W |
| A Optics | Central Wavelength | 1080 ± 10nm |
| A Optics | Pulse Width | 30-500ns (Adjustable) |
| A Optics | Repetition Frequency | 1-4000kHz (Adjustable) |
| A Optics | Single Pulse Energy | 1.5 / 2 / 5 / 10 / 15 / 50 / 100mJ |
| A Optics | Laser Brand | JPT (Standard) |
| A Optics | Fiber Length | 5m / 10m (Optional) |
| B Cleaning | Cleaning Efficiency | > 30 m²/h |
| B Cleaning | Max Working Area | 1200 x 1200mm (Customizable) |
| B Cleaning | F-Theta Lens | F300mm (DOF 15-25mm) |
| B Cleaning | Actuator Mechanism | Gantry + 5-Axis / 6-Axis Linkage |
| B Cleaning | Applicable Materials | Carbon Steel, Stainless Steel, Aluminum, Copper, Mold Steel, Stone, Wood |
| B Cleaning | Rust Removal Grade | Sa2.5 / Sa3 |
| C Motion | Structure | Dual-Drive Gantry (Large Format) |
| C Motion | Effective Stroke (X+Y+Z) | Fully Customizable |
| C Motion | Repeat Accuracy | ±0.01mm |
| C Motion | Motion Axes | 3-Axis Standard (5/6-Axis Optional) |
| C Motion | Guide Rails | HIWIN / THK / PMI |
| C Motion | Transmission | Linear Guide (X+Y) + Ball Screw (Z) |
| C Motion | Servo System | Delta / Inovance / Panasonic / Yaskawa |
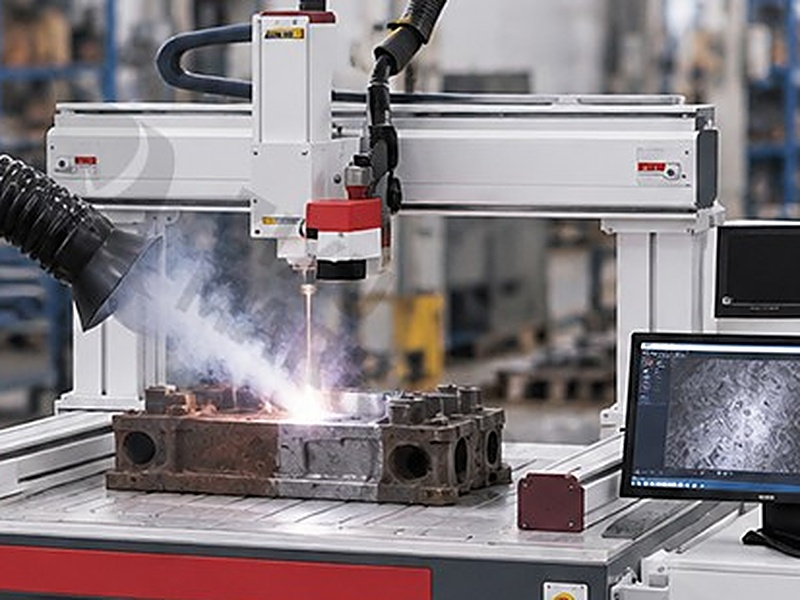
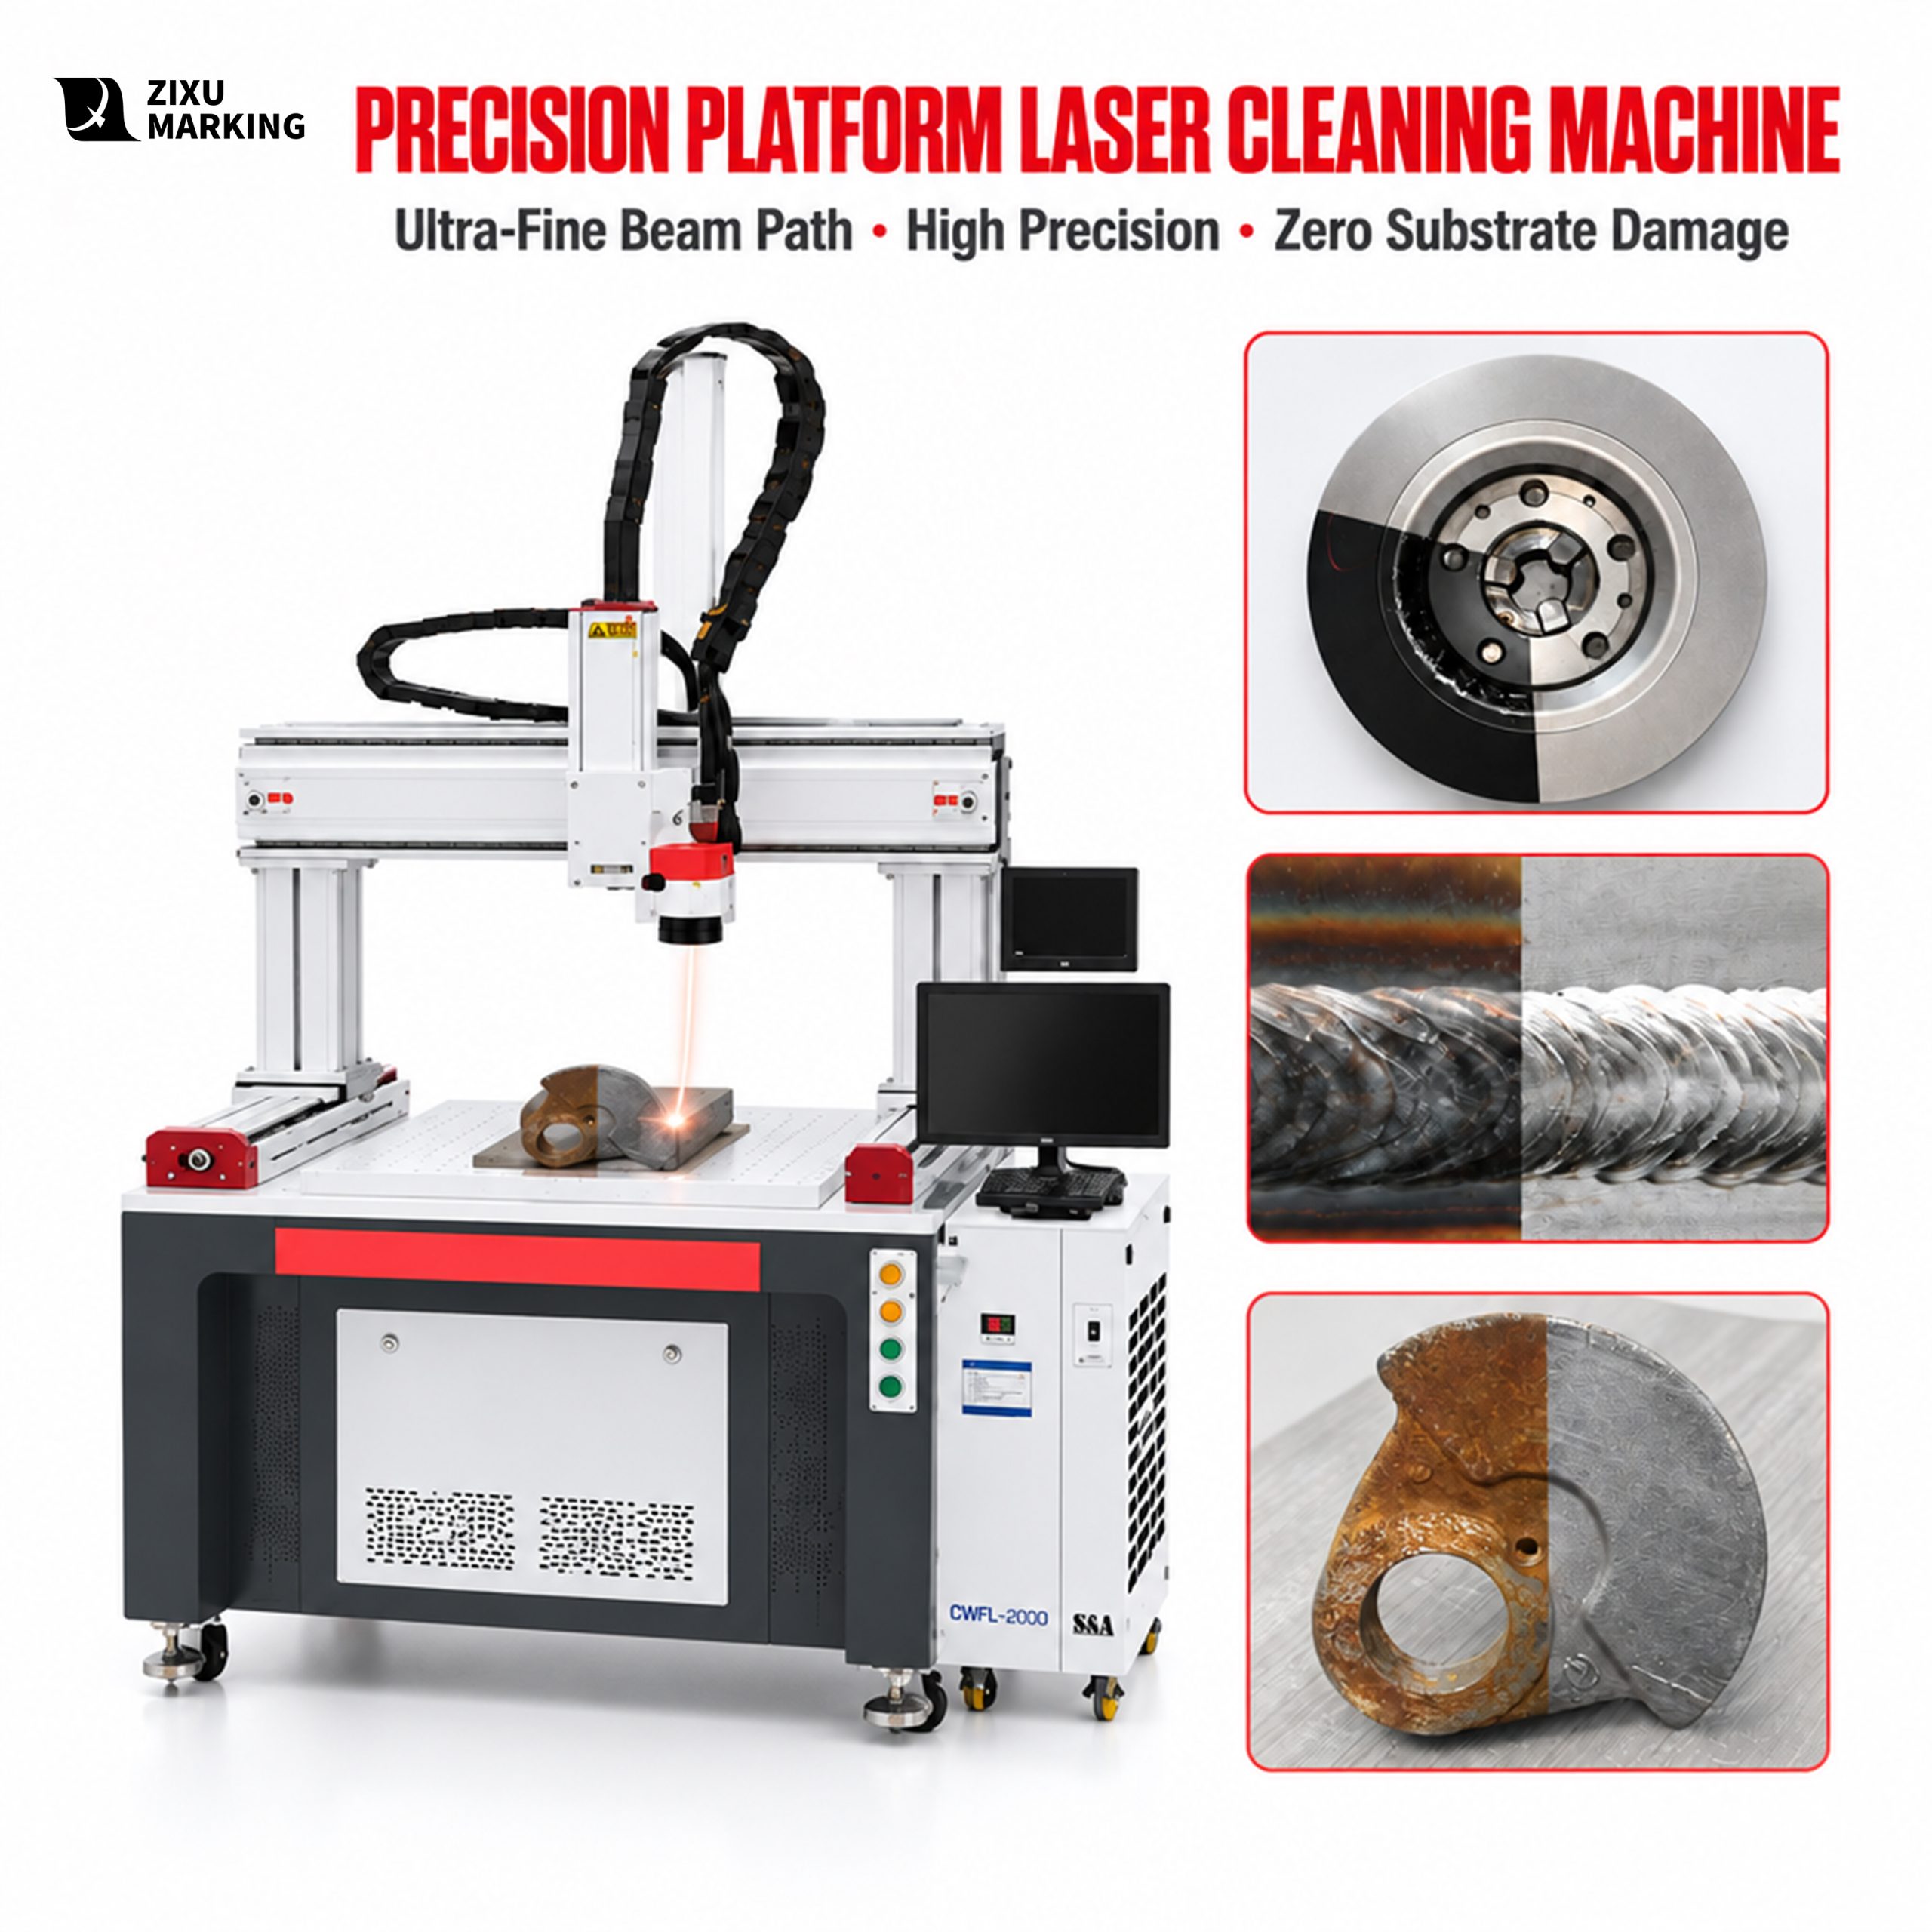
Dual-drive gantry on linear guides: accuracy comes from the structure
A servo at each end of the beam, linear guides on X/Y (HIWIN / THK / PMI), a ball screw on Z, and +/-0.01 mm repeatability. The gantry carries the galvo anywhere over the table without losing stiffness with distance, which is why the same line quality holds at 200 mm and at 1200 mm.
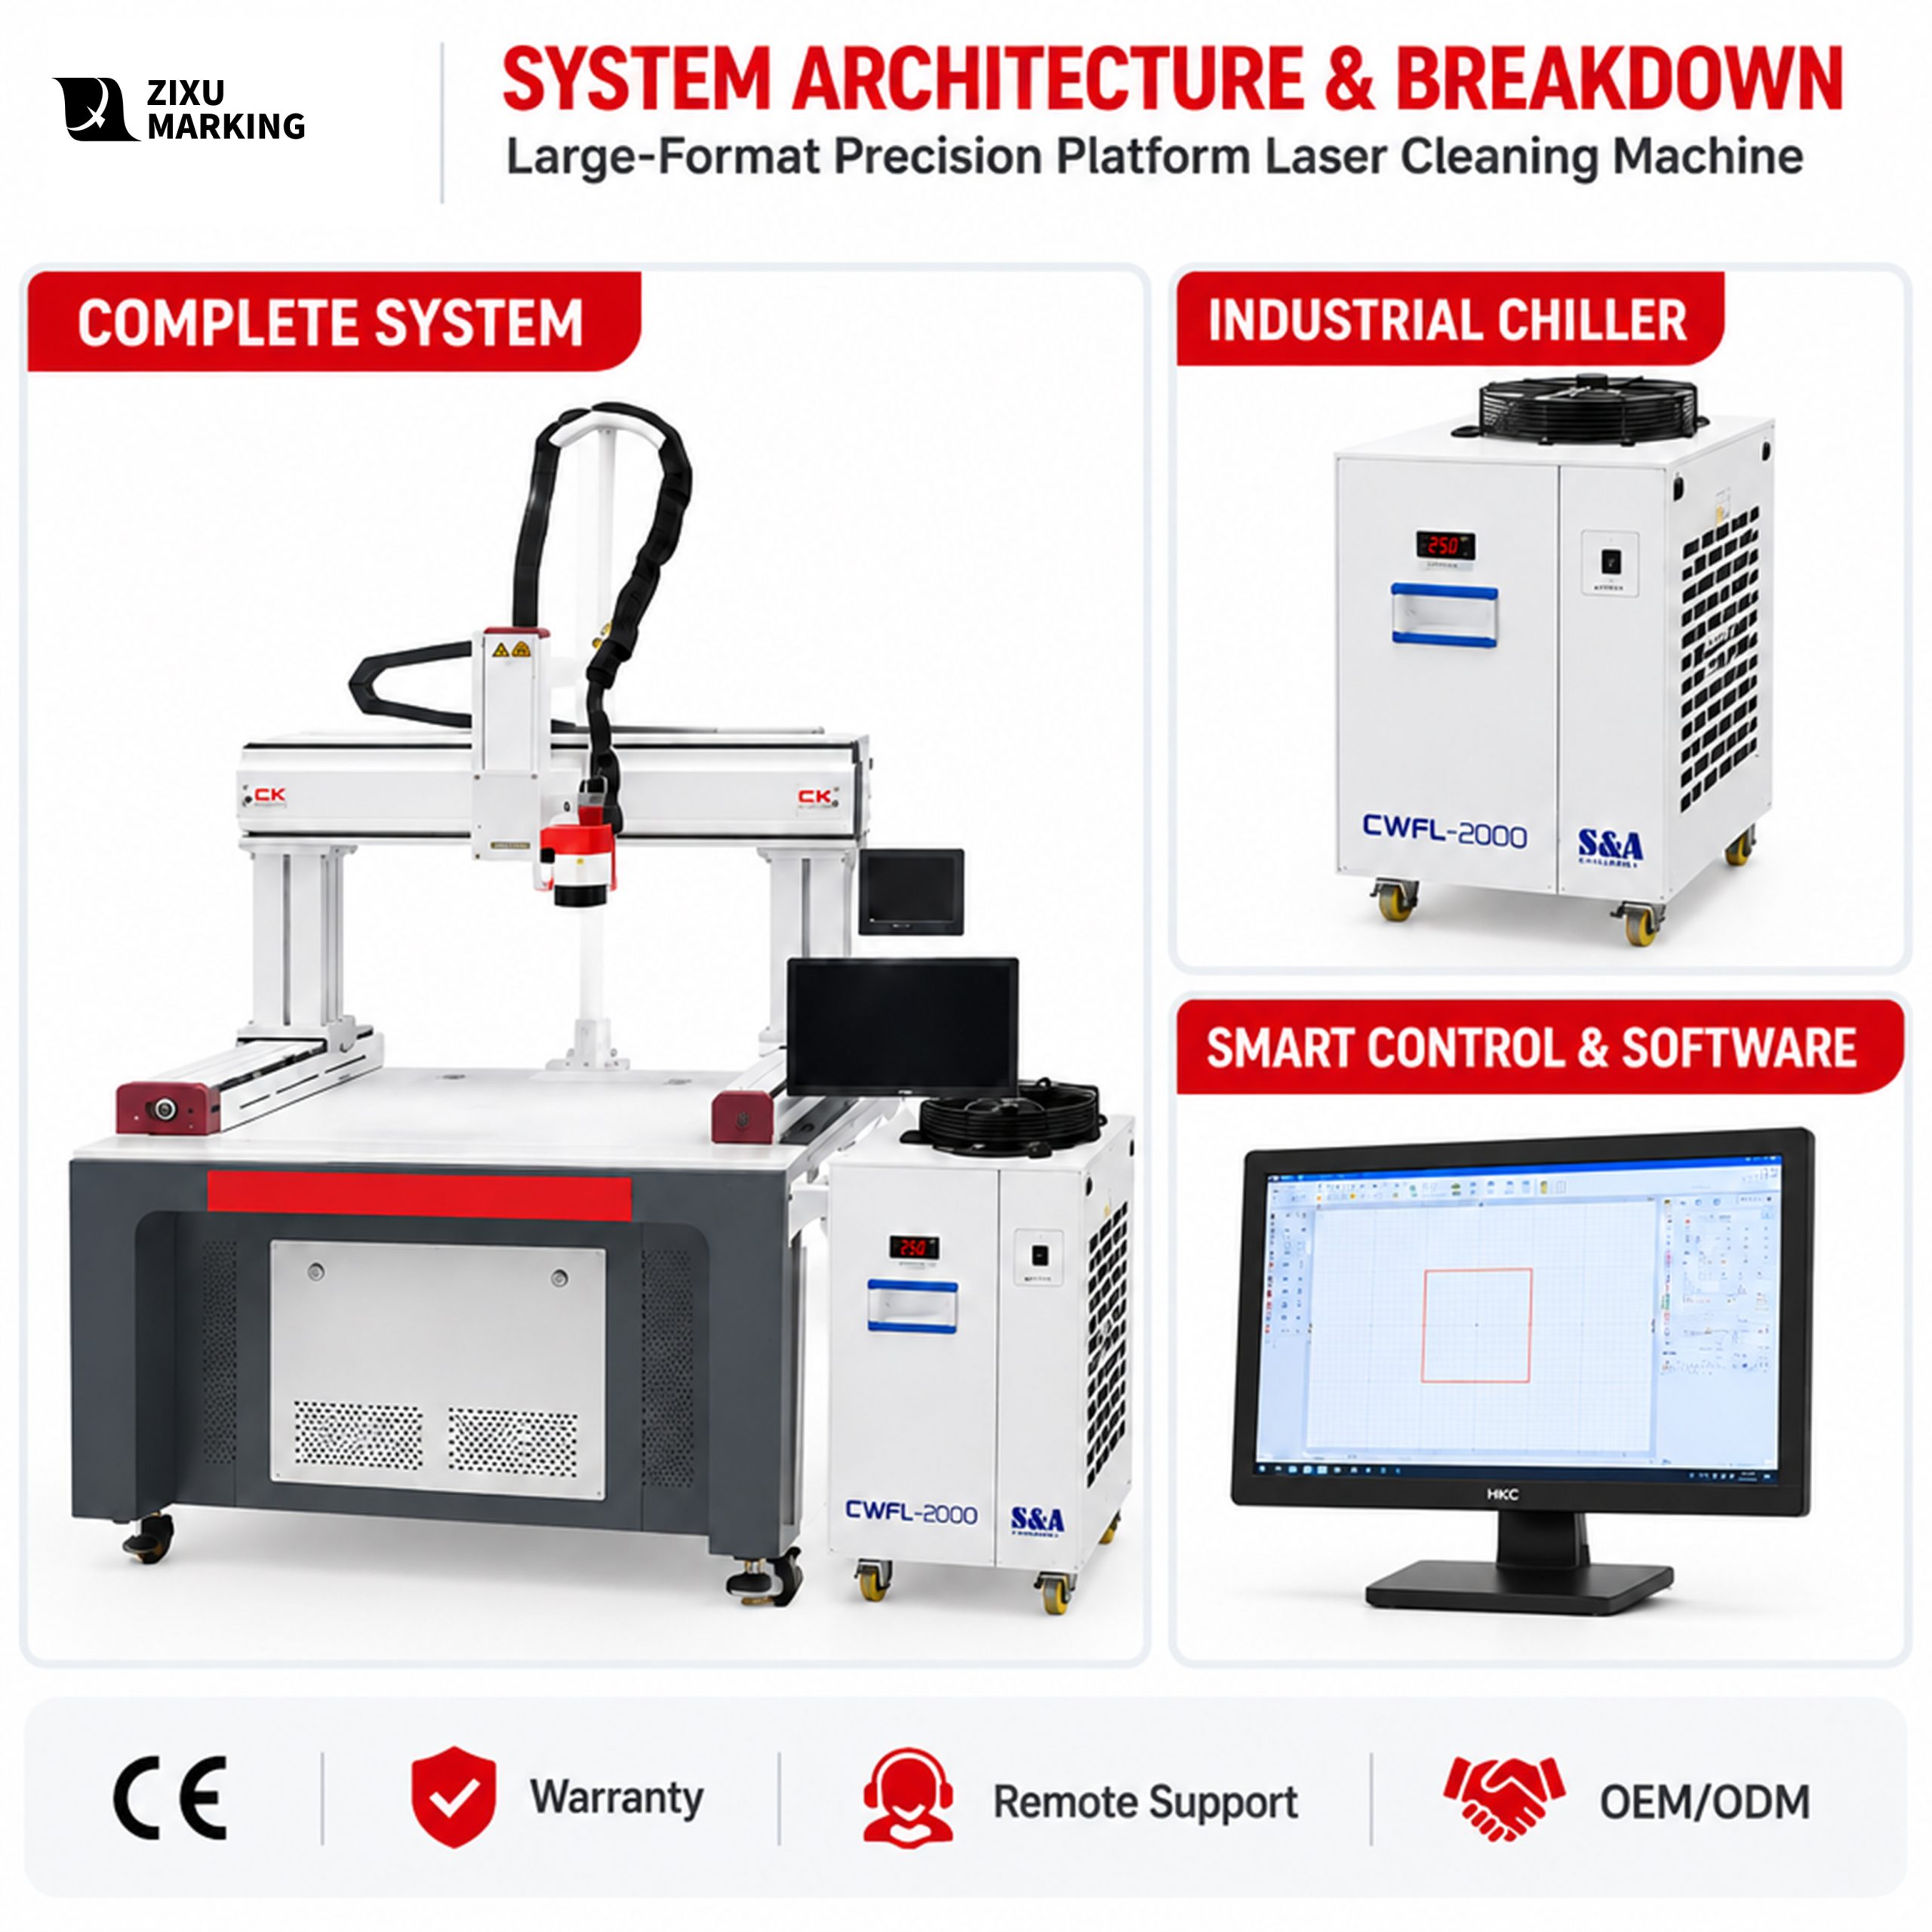
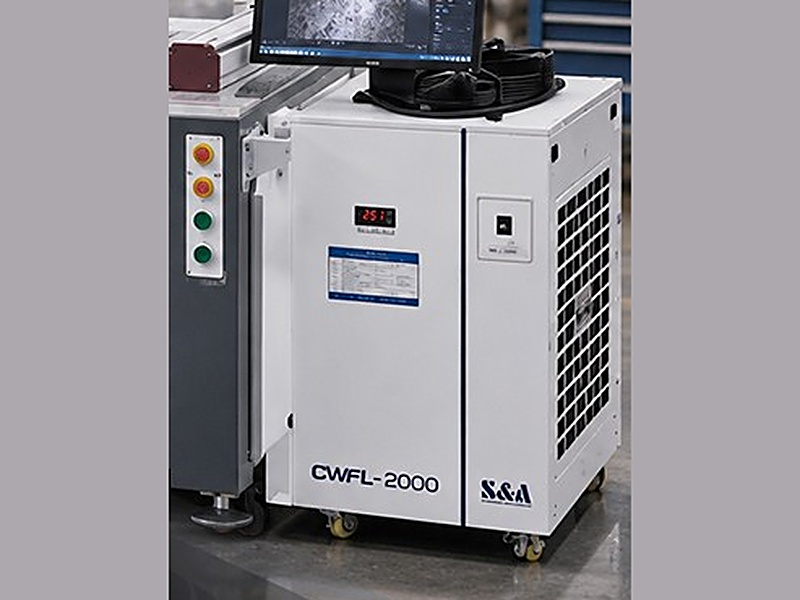
S&A CWFL-2000 chiller: visible temperature, stable power
The CWFL-2000 beside the cabinet is a dedicated laser chiller reading 25.1 C on its own display. At the 1000 W level water temperature translates directly into power drift and lens life; air cooling cannot hold this range. It is not an option, it is the entry ticket.
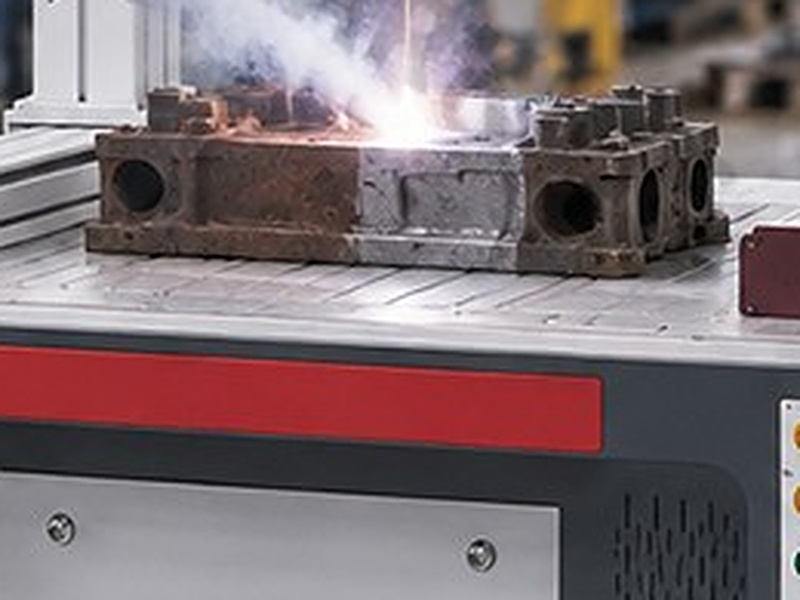
A 1200×1200 table: clamp the part, run it once
The part is clamped to the table while the gantry runs an F300 lens (15-25 mm depth of focus) over the whole face, with an extraction hose taking the plume away. One set-up covers rust, paint and oxide in the same program, with no flipping and no hand touch-up.
Recipe library: a different operator, the same result
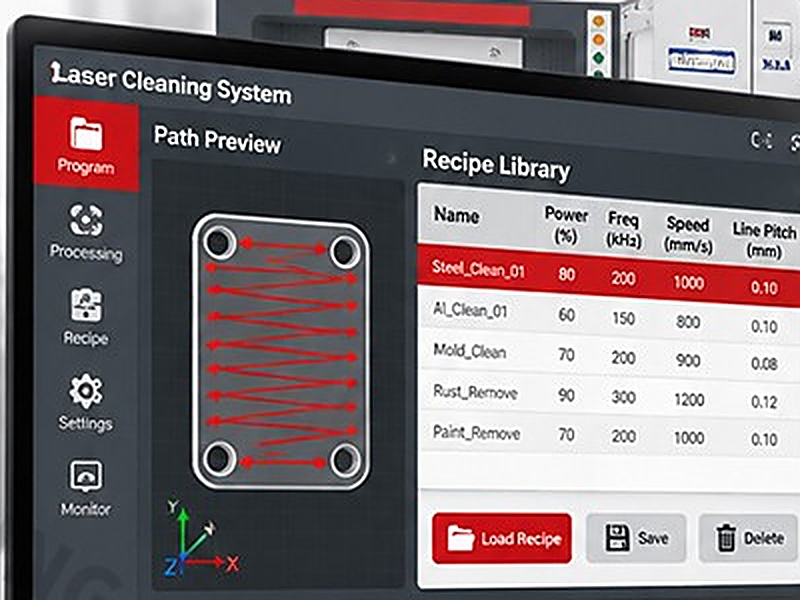
The screen shows a recipe table: power percentage, frequency, scan speed and line pitch per material, recalled with Load Recipe. Once locked, batch variation collapses to the +/-0.01 mm the machine holds – the certainty a handheld unit cannot offer.
Cross-section: clean surface, intact metal below
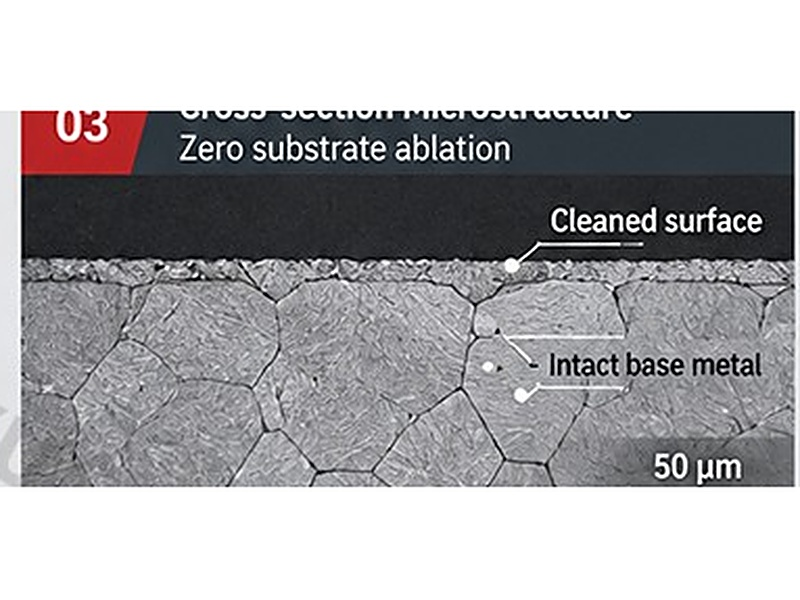
At a 50 micrometre scale the section shows the cleaned surface above and untouched base metal below, with a flat interface and no ablation pits or heat-affected layer. That is the evidence behind non-contact: it is what lets a thin-wall or precision part be cleaned this way.
Real parts: four materials, one clean boundary
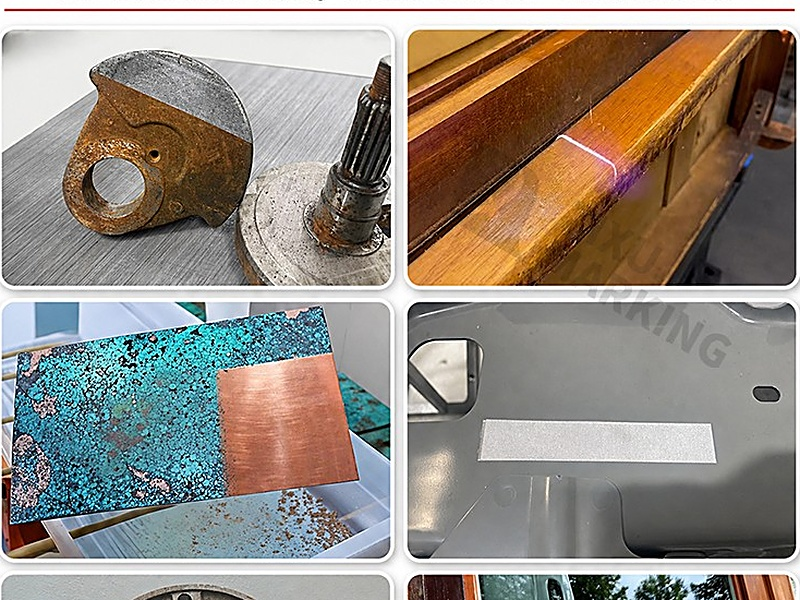
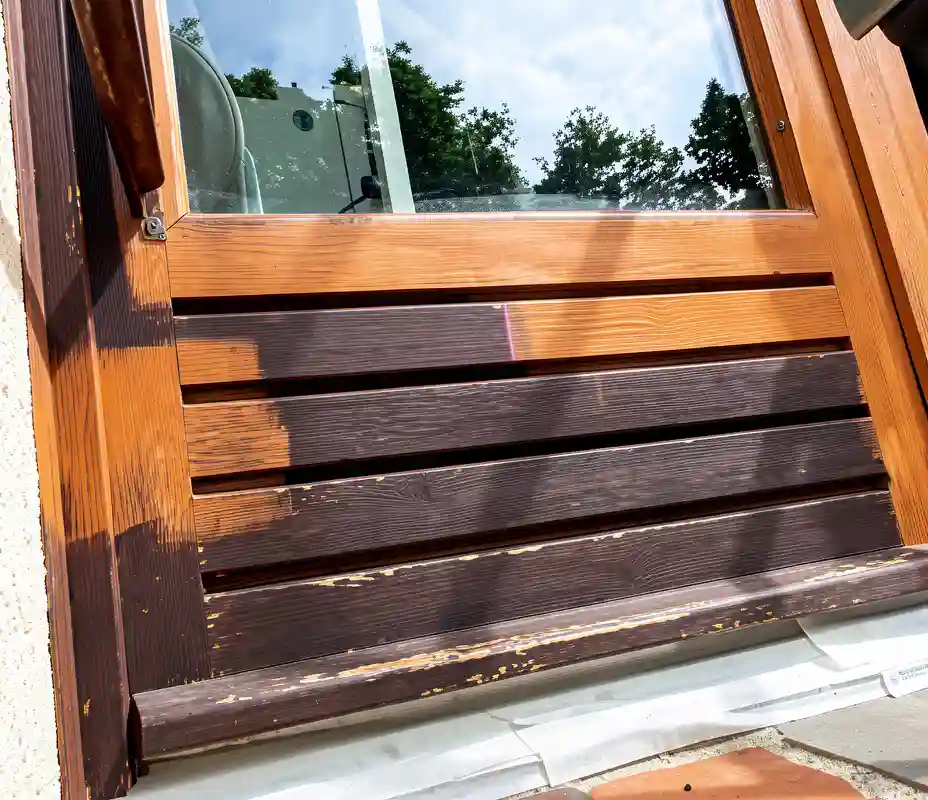
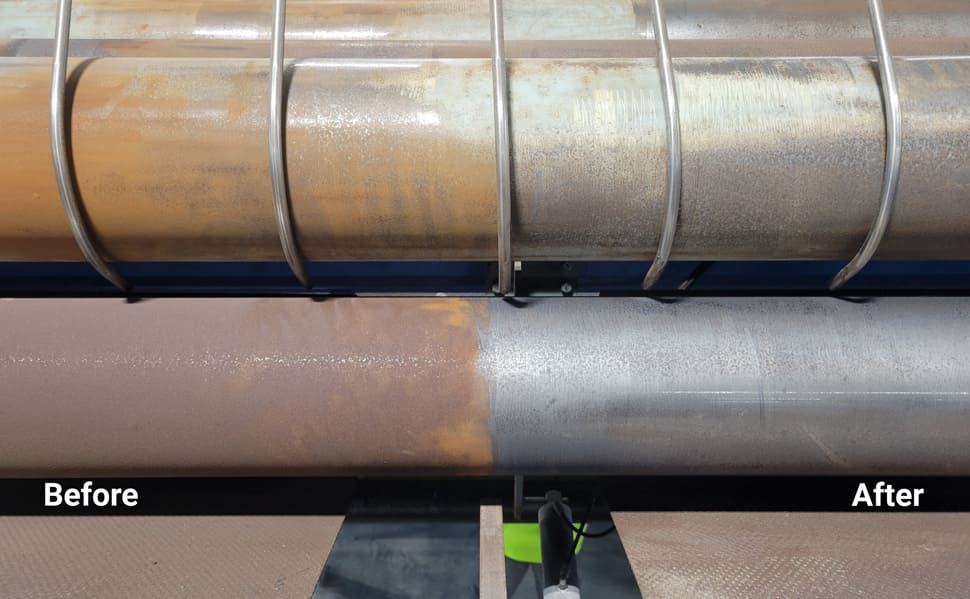
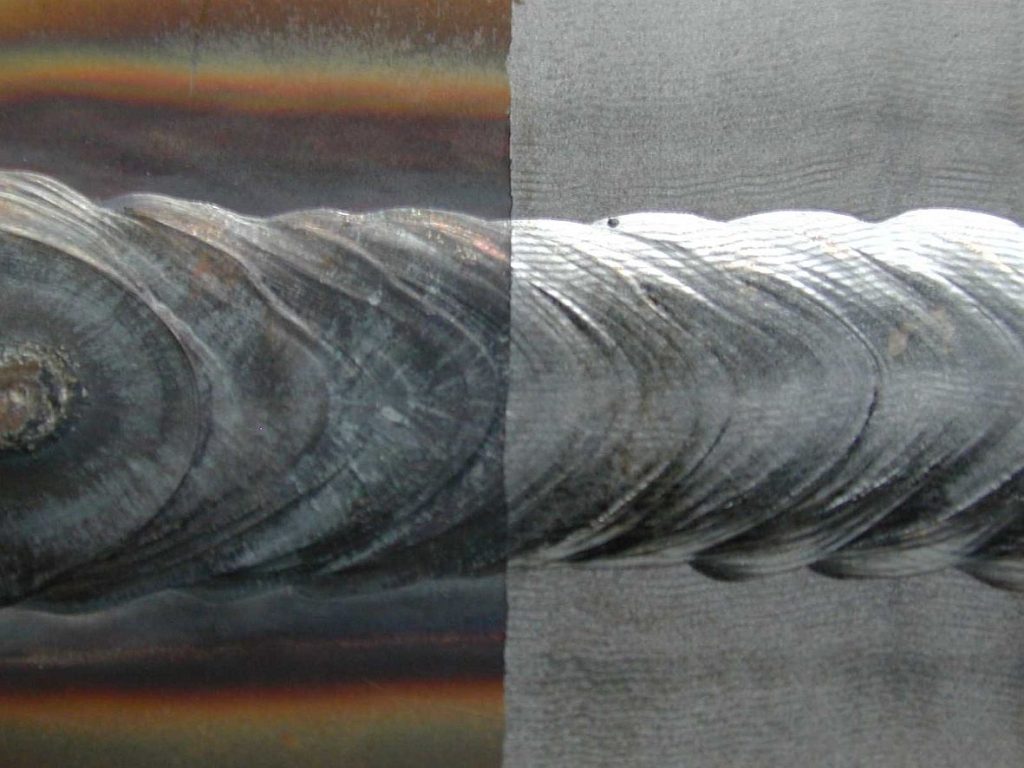
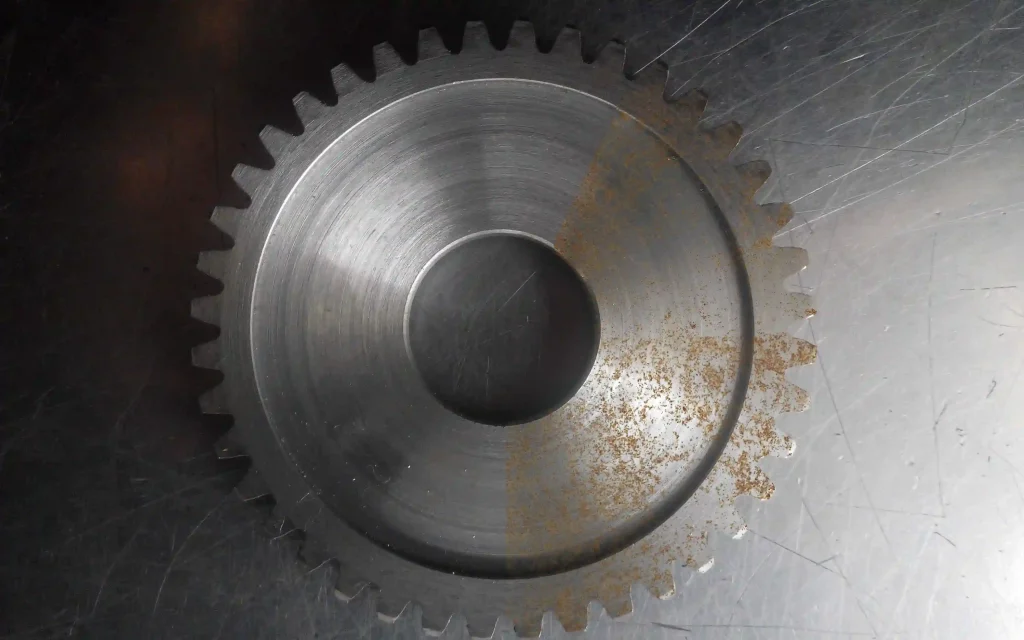
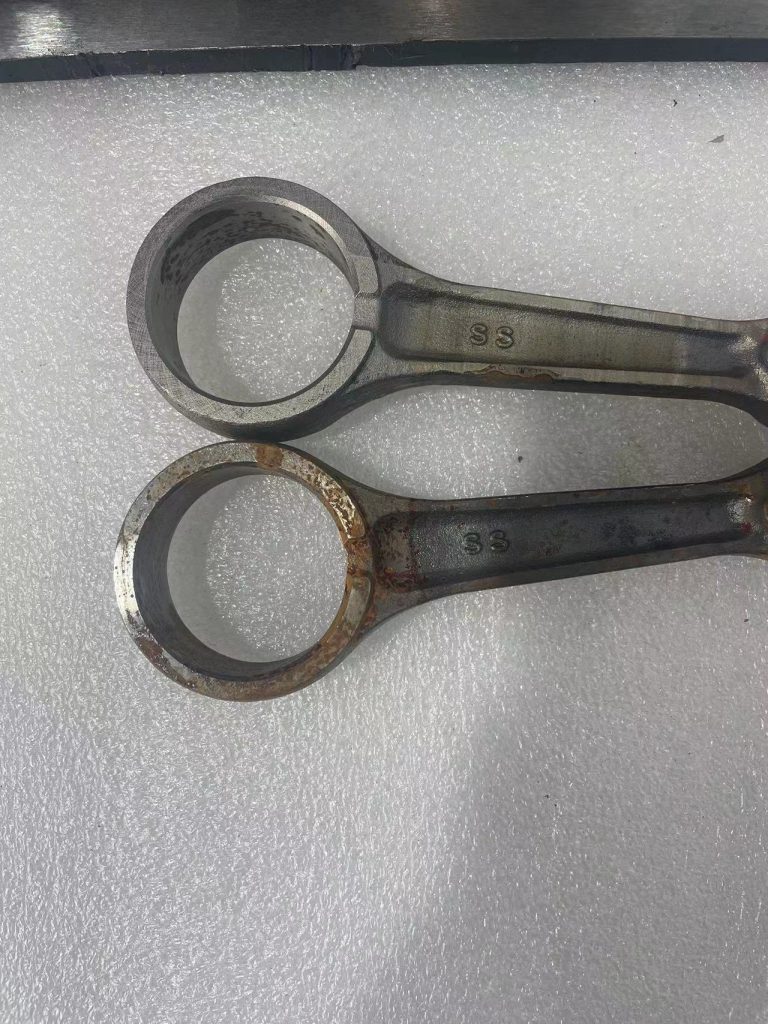
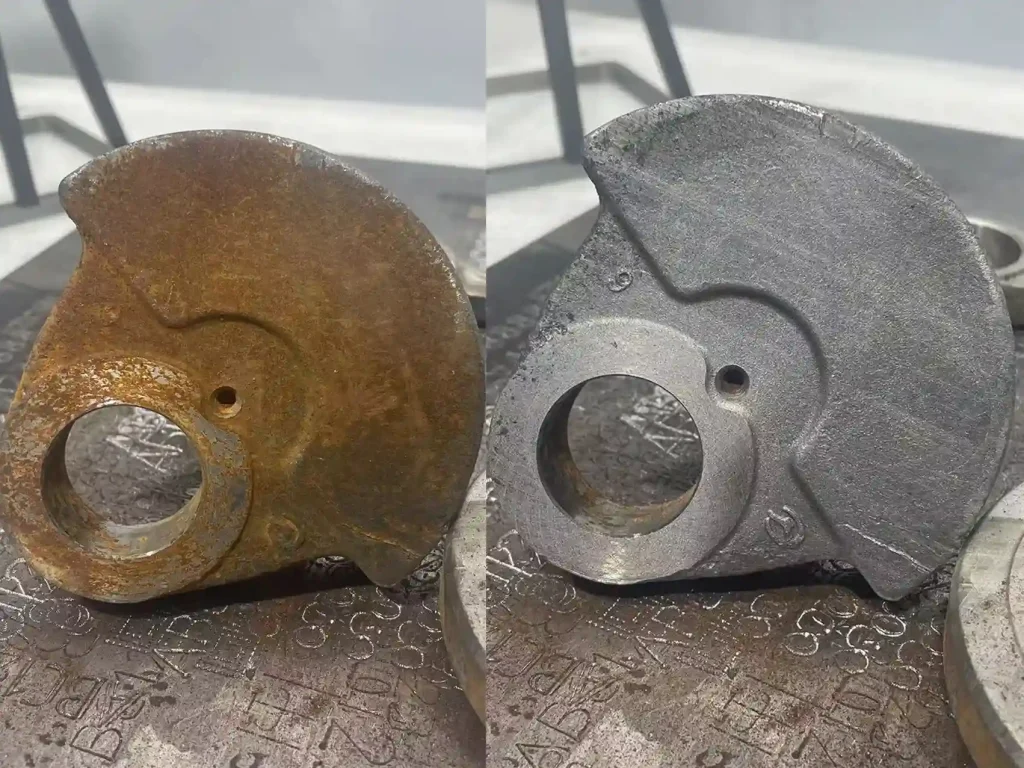
Cast iron derusted, a timber beam stripped, copper de-oxidised, paint removed from sheet – four substrates and four contaminants, with the boundary stopping where the program set it and the substrate texture untouched. Same machine, same parameter logic.
Material Compatibility
| Material | What it removes | Note |
| Carbon and cold-rolled steel | rust removal to Sa2.5 / Sa3 | take heavy rust in passes |
| Stainless | heat tint, weld discolouration, oil | clean both sides before welding |
| Aluminium | oxide, release agent | low power, high frequency |
| Copper | oxide, oil | high reflectivity, more power needed |
| Mould steel | carbon build-up, release residue | tyre moulds; 5-axis for cavities |
| Stone and wood | deposits, old coatings | wood: low power, fast travel |
Cutting Samples
Send us an email to get further information you need, including our latest price, the best-customized solution, or any problem with the existing machine.