Automatic Gantry Five-Axis Fiber Laser Welding Machine for Stainless Steel, Carbon Steel and Aluminium
A gantry table with five interpolated axes and a 1500-6000 W CW fibre source: X, Y and Z carry the torch, Rotary and Tilting set its angle, RTCP holds focus through the turn, and wire feeding runs 0.8-2.0 mm on 0.4 MPa air or argon.
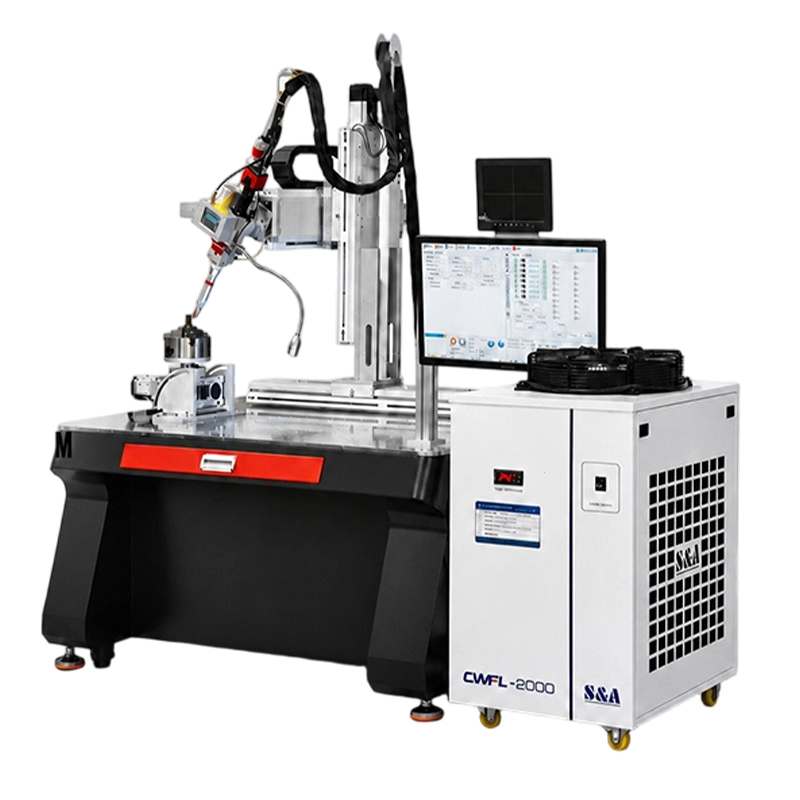
1500, 2000, 3000 or 6000 W CW at 1080 +/-5 nm, with 0.8, 1.0, 1.2, 1.6 or 2.0 mm filler, fed as single, dual or triple wire at 30-600 mm/s. Power sets penetration on thick sections; the wire sets how much gap the fixture has to close. The feeder mounts to the torch, so ordering it with the machine costs less than retrofitting it.
0.4 MPa compressed air, argon or nitrogen, delivered coaxially, from the side, or both. Air is enough for carbon steel. Stainless and aluminium need argon, or the bead blackens and porosity climbs. Galvanised sheet needs side blowing so zinc fume never crosses the beam.
The water circuit is built into the cabinet: one set of connections in and out, no chiller standing on the floor. That is what lets a 1080 nm source run at rated power all shift. On a table that welds by the hour, an air-cooled 1500 W unit de-rates; a water-cooled 6000 W does not.
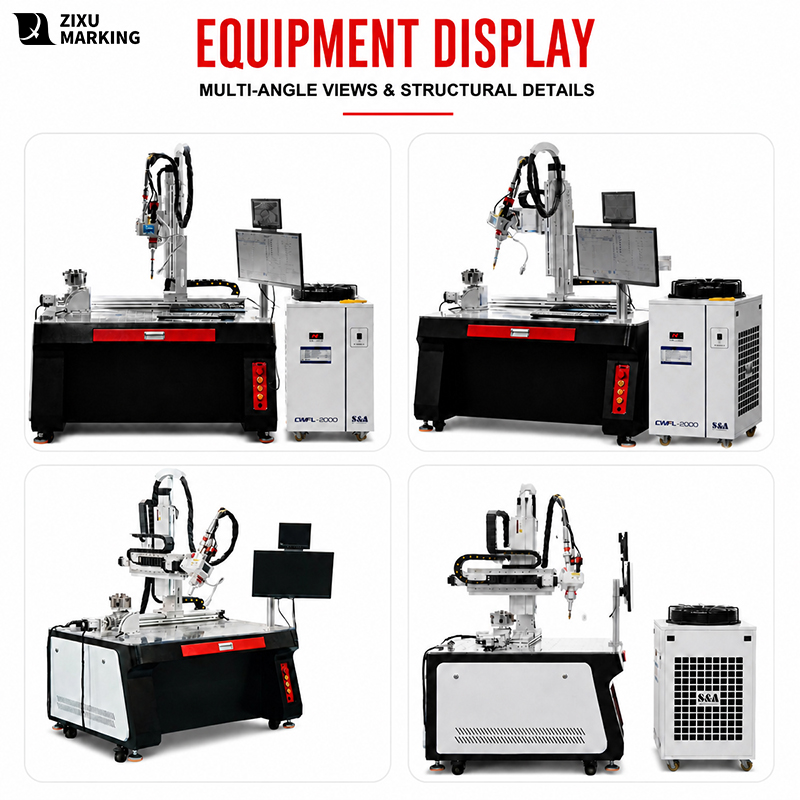
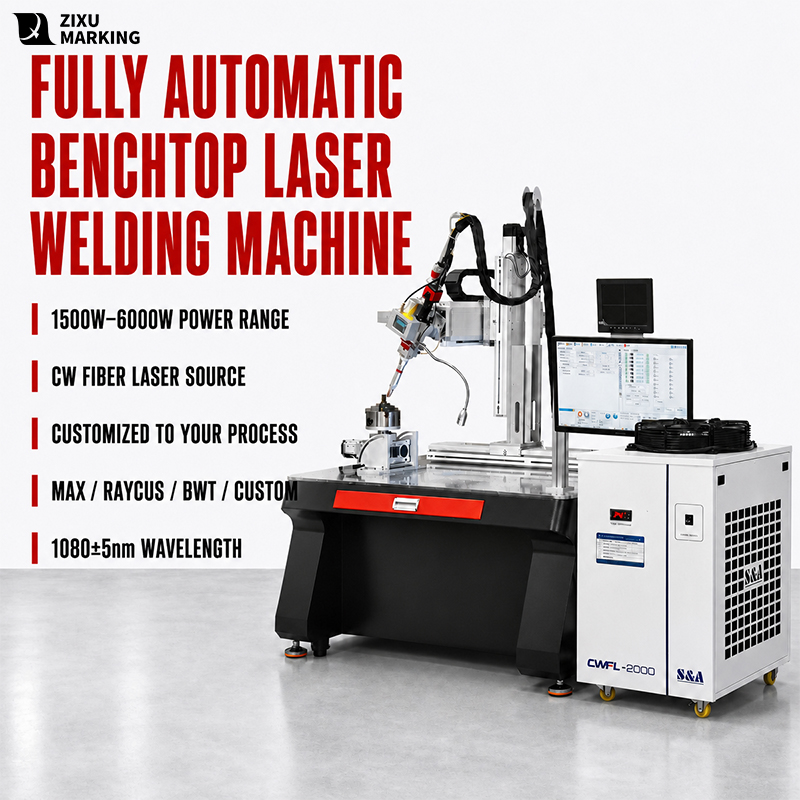
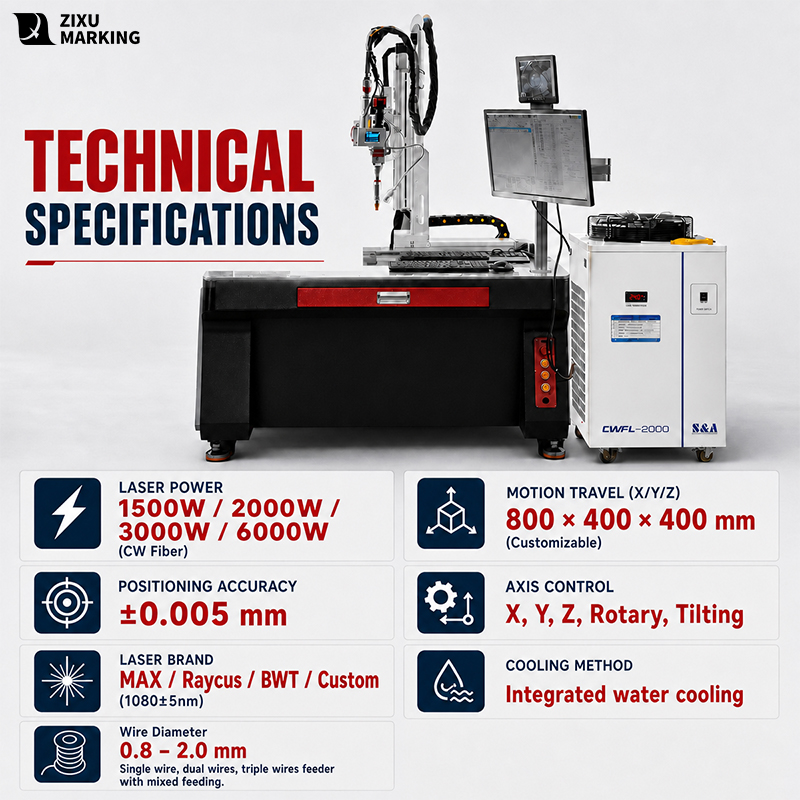
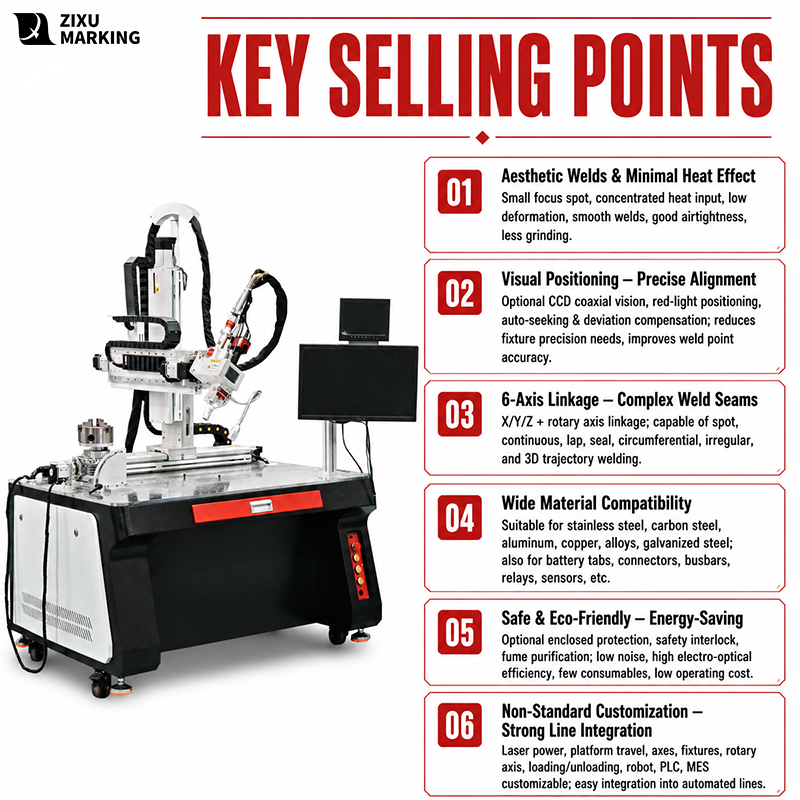
An 800 x 400 x 400 mm gantry with five interpolated axes: X, Y and Z carry a 1500-6000 W CW fibre source at 1080 nm, while a rotary axis and a tilting head set the angle of the joint. Rails and beam are dual-drive servo on linear guides, the moving modules hold +/-0.005 mm, and RTCP keeps the focal point on the seam while the axes turn, so defocus and incidence stay constant through a curve. Filler runs 0.8-2.0 mm through single, dual or triple feeders; shielding is 0.4 MPa air, argon or nitrogen, coaxial, side or mixed. Water cooling sits inside the cabinet and the controller takes CAD geometry directly, so a new part is programmed while the table keeps welding. Travel is 800 x 400 x 400 mm as standard and built to drawing beyond that.
| Parameter | Specification |
| Laser Type | CW Fiber |
| Laser Brand | MAX, Raycus, BWT or customize |
| Laser Power | 1500W / 2000W / 3000W / 6000W |
| Laser Wavelength | 1080 ± 5nm |
| Axis Control | X, Y, Z, Rotary, Tilting |
| Travel Length of Motion | 800 * 400 * 400mm or customize |
| Moving Module Accuracy | ±0.005mm or customize |
| Wire Diameter | 0.8mm, 1mm, 1.2mm, 1.6mm, 2mm |
| Optional Feeder | Single wire, dual wires, triple wires feeder with mixed feeding. |
| Feeding Speed | 30 – 600mm/s |
| Cooling Method | Integrated water cooling |
| Air Supply | 0.4MPa compressed air or protective Argon, Nitrogen, etc. |
| Air Blowing Mode | Coaxial blowing, side blowing or mixed blowing. |
Features
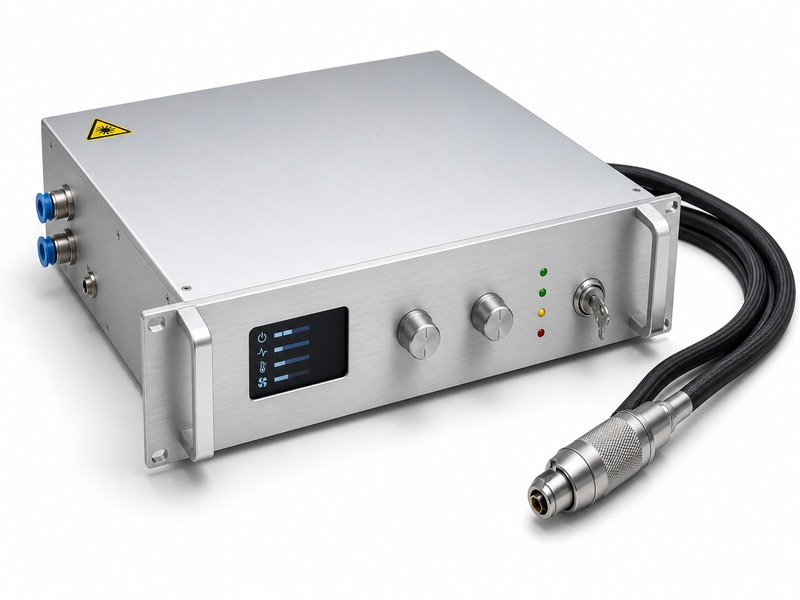
The source sets the ceiling on machine life
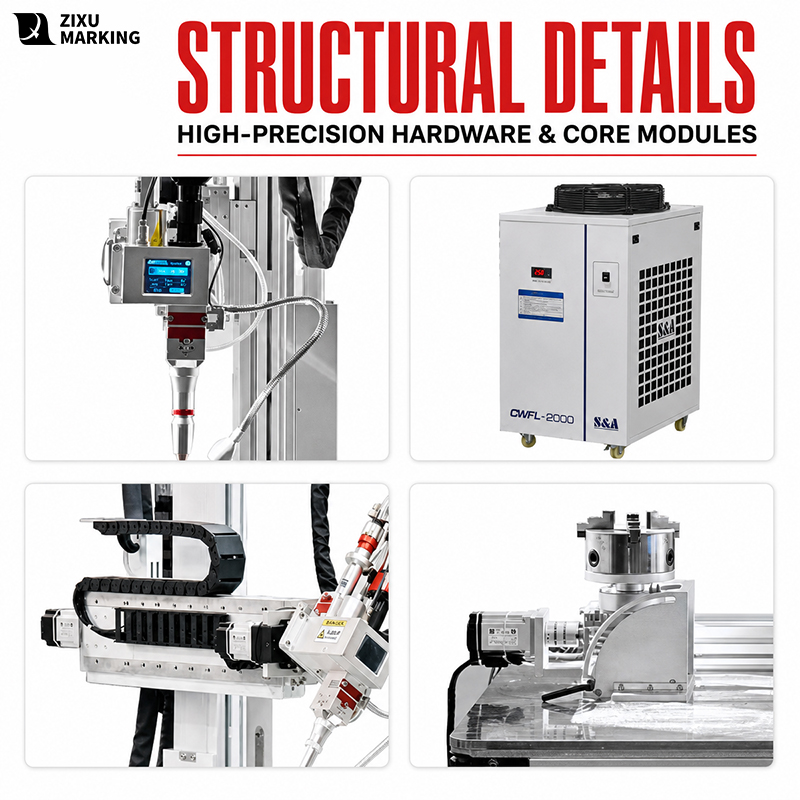
Continuous-wave fibre source in four steps – 1500, 2000, 3000 or 6000 W at 1080 +/-5 nm – with the brand settled between MAX, Raycus and BWT by lead time. It sits inside the base, and it is the one part that stops the whole machine when it fails, which makes it the last part to buy at the bottom of the price list. Power is sized against the thickest joint in the drawing: 1500 W covers thin sheet, but pointed at 5 mm structural steel it produces for three months and then shortens its own life.
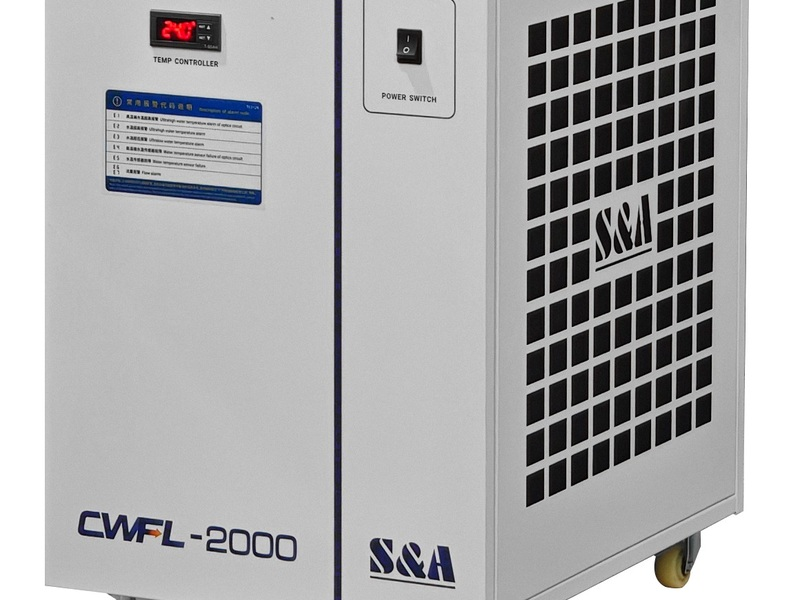
The chiller states its own nameplate
The unit fitted is the S&A CWFL-2000, matched to a 2000 W source, with a temperature display (24.0 C in this shot), an alarm-code chart and its own power switch on the front panel. A one-degree drift in water temperature is enough to move the operating point of the source and the collimating lens: on thin sheet it shows as penetration that wanders, and over a year as condensation on the optics. It stands outside the cabinet, so servicing needs no strip-down – and of ten same-price machines we sampled, zero named a chiller brand.
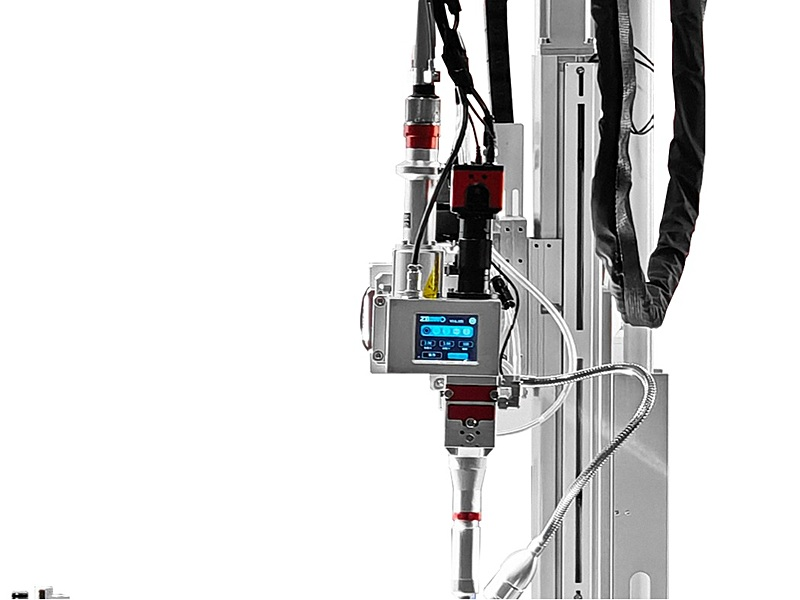
Column and linear guide: the stiffness is in the rail, not in a wrist
The torch rides a linear guide on a single column and is lifted by the carriage, with a cantilever arm reaching the work position; the column is aluminium profile with a steel rail, and the whole cable set runs in a drag chain instead of hanging across the beam path. Moving modules hold +/-0.005 mm over an 800 x 400 x 400 mm travel, larger built to drawing. Against an articulated robot, error here does not grow with reach: a longer machine means a longer rail, not a softer posture.
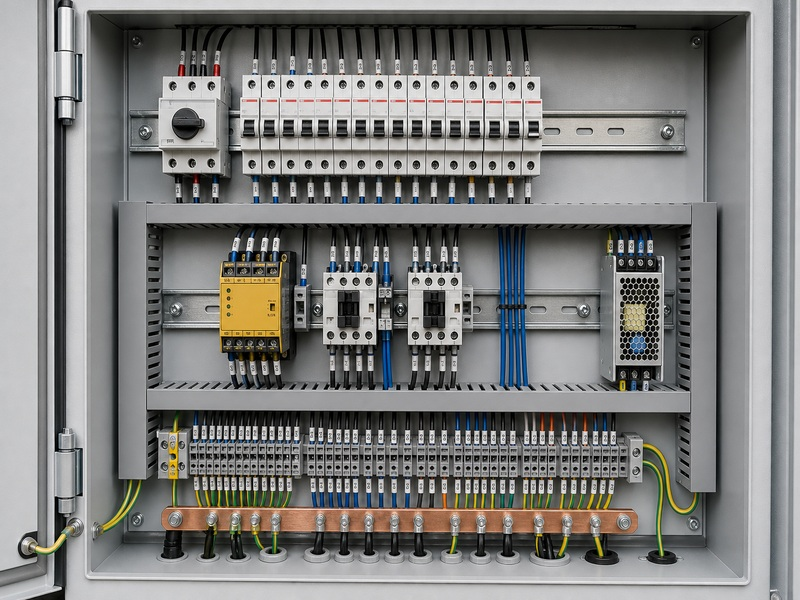
The electrical cabinet: where most failures start, and the last thing anyone photographs
The cabinet is laid out by circuit: breakers and the main switch on one rail, safety relay and contactors on the next, numbered terminals, ferrules on every core, a copper earth bar along the bottom. Around eighty percent of welding-cell faults are electrical – a loose terminal, a welded contactor, a poor earth. Cables dressed and numbered turn diagnosis into ten minutes; a loom turns it into half a day. Of ten same-price machines sampled, exactly one showed the inside of its cabinet.
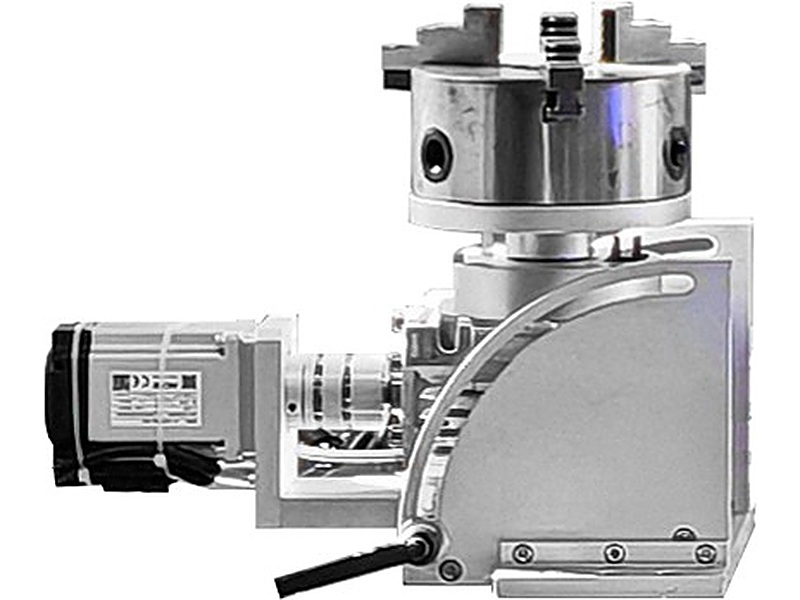
Rotary fixture: servo, planetary gearbox, three-jaw chuck
A servo drives a planetary gearbox through a coupling, and the gearbox turns a three-jaw chuck; the work is clamped in the chuck and indexed by the C axis. Circular seams on tubes, flanges and shafts come off this axis while the torch holds its attitude – roundness is set by the fixture’s rotational accuracy, not by an operator compensating. Chuck and gearbox are standard parts, so jaws or a gearbox can be replaced without waiting on the machine builder.
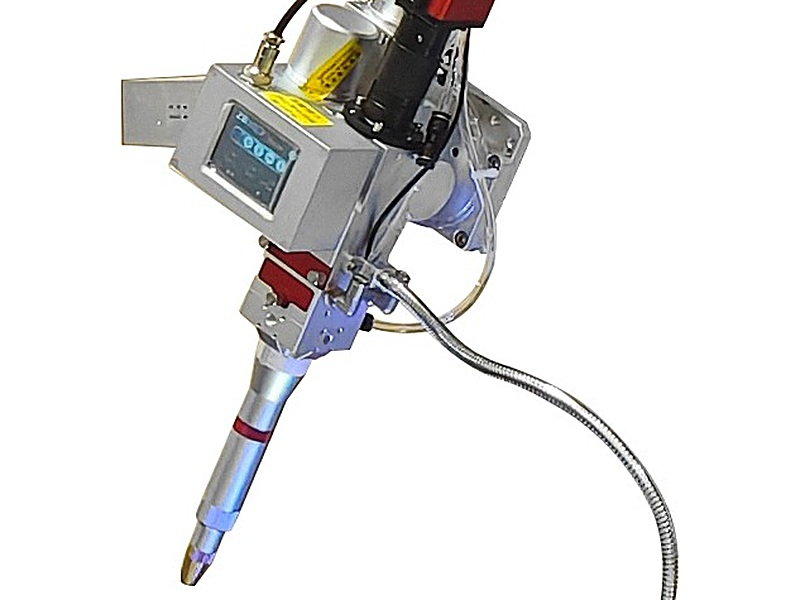
Torch: its own display, and only three wearing parts
The torch body carries a small display so power and process parameters are readable at the joint instead of on the main screen; below it sit the protective lens holder and the copper nozzle, with the shielding line entering from the side and the wire guide on the flank. Only three parts on the machine wear: the lens, the nozzle and the feed roll. The lens is retained by its own cap on the outside of the head, so changing it needs no strip-down and no refocusing – which buys back downtime and removes the temptation to keep welding through a dirty lens.
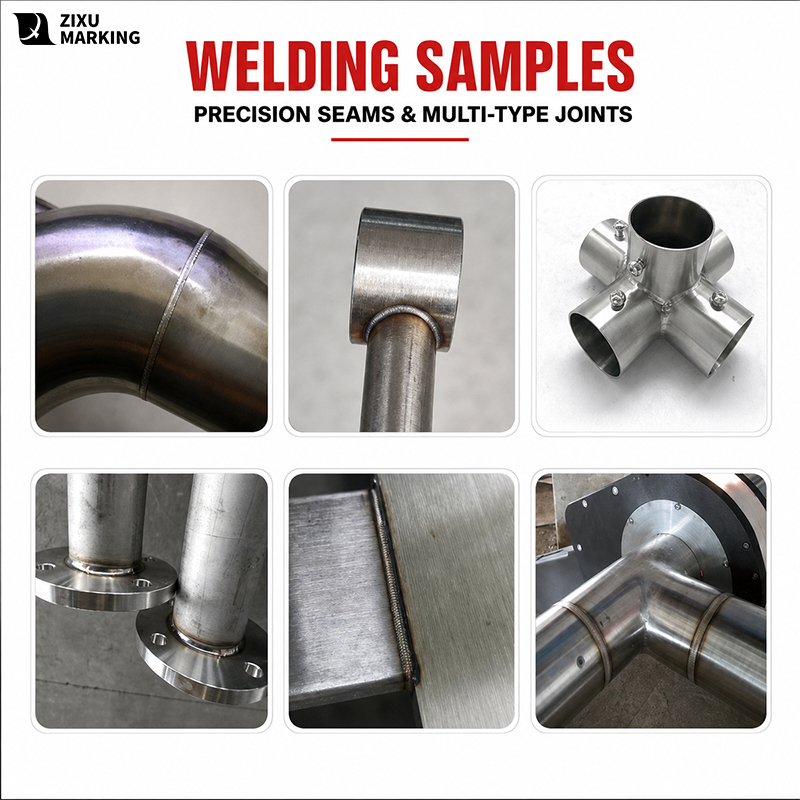
Material Compatibility
| Material | Typical joint | On the page | Power and shielding to start from |
| Carbon steel | Box sections, frames, structural butt joints | On the page | Air shielding is enough; 1500-3000 W for 1-6 mm, 6000 W with a bevel for thicker plate |
| Stainless 304 / 316 | Cabinets, trays, tube assemblies | On the page | Argon with back purging, or the bead goes black and the root oxidises |
| Aluminium alloys | Battery trays, housings, extrusions | On the page | High reflectance and fast heat conduction: more power density plus argon; thin wall on a low-current continuous mode |
| Galvanised steel | Sheet-metal parts, brackets | On the page | Zinc fume disturbs the beam, so side blowing is mandatory; lap gap under 10 percent of sheet thickness |
| Copper / brass | Busbars, heat sinks, connectors | On the page | Absorption at 1080 nm is low: 3000-6000 W at speed, and sample first |
| Titanium alloys | Aerospace and chemical parts | Not on the page | Full inert shielding with a trailing shield; sample before promising porosity |
Marking Samples
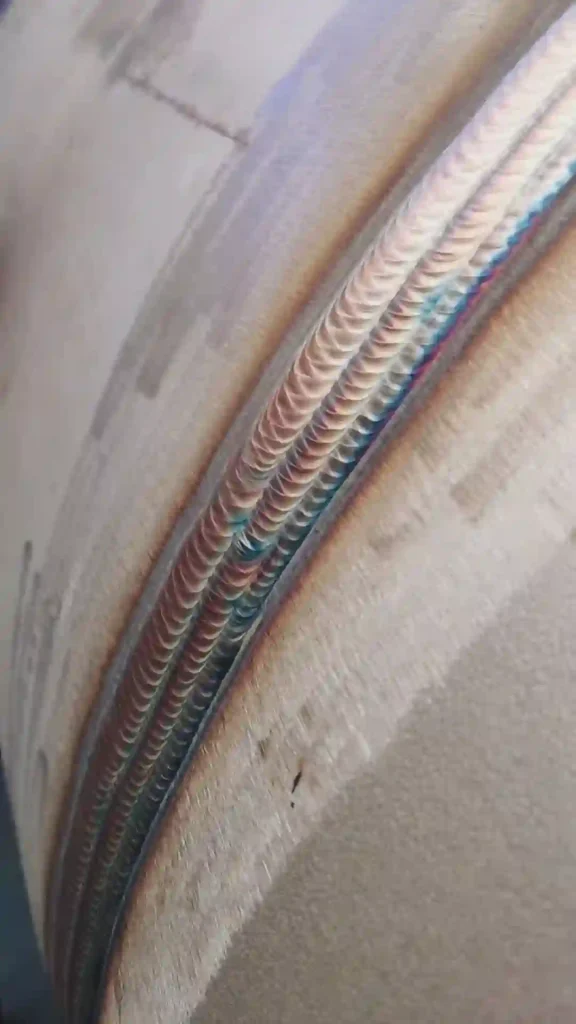
Related Products
Send us an email to get further information you need, including our latest price, the best-customized solution, or any problem with the existing machine.